
UTP Maintenance, stick electrode, nickel alloys

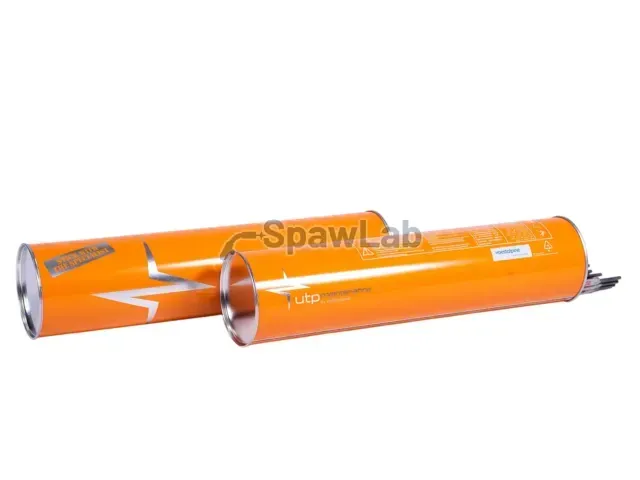
UTP 7015 NK stick electrode

EN ISO classificationEN ISO 14172: E Ni 6093 (NiCr15Fe8NbMo)
AWS classificationAWS A5.11 / SFA-5.11: ENiCrFe-3 (mod.)
Price on request
Give us the diameter and the quantity, we will quote during working hours

Spawlab is the data controller. We will use your data only for replying to this price enquiry. See the privacy policy for details.

Authorised distributorvoestalpine Böhler Welding
Courier shippingfrom the warehouse in Krotoszyn
Data sheetcomposition, properties, specifications
Wire selectionhelp from a welding engineer
Manufacturer data sheet
Application

What UTP 7015 NK stick electrode is used for

UTP 7015 NK is a basic coated nickel base electrode of the E Ni 6093 / ENiCrFe-3 (mod.) type. The manufacturer intended it for repairs and for joining heat resistant nickel alloys, steels for low temperature service, joints between low alloy and stainless steels, and steels of difficult weldability. It also suits a ductile buffer layer under hard surfacings of nickel and cobalt alloys.

The deposit has an austenitic structure, it does not turn brittle at high or at low temperature, it resists corrosion and it work hardens: the manufacturer states about 180 HB as welded and about 350 HB once work hardened. The arc burns calmly, the slag comes away well and the weld face has a fine ripple with no notch at the toes.

  • Classification EN ISO 14172: E Ni 6093 (NiCr15Fe8NbMo)
  • AWS classification A5.11 / SFA-5.11: ENiCrFe-3 (mod.)
  • Coating: basic
  • Current: DC+
  • Diameters: 2.0 / 2.5 / 3.2 / 4.0 mm
  • Lengths: 300, 350 and 400 mm

On hard to weld steels of unknown composition this electrode gives you a safety margin, but preheat the part all the same and let it cool slowly. Under hard surfacing lay one or two buffer layers and only then the wear resistant alloy. Keep the current low and the beads narrow, because an austenitic deposit shrinks strongly. You can peen the repaired surface afterwards, to make use of the work hardening.

Manufacturer datasheet

Chemical composition and properties from the manufacturer datasheet

Datasheet PDF

Typical weld metal values from the voestalpine Böhler Welding data sheet, issue 04/2023. The minimum or the range guaranteed by the maker is given in brackets. The figures depend on the heat treatment condition and the shielding gas stated in the row and do not replace testing the joint to your own WPS.

Chemical composition, wt.-%
CSiMnCrNiMoNbFe
0,030,44,515balance1,227
Welding data and approvals
Polaritydirect current, electrode positive (DC+)
Datasheet edition04/2023
Fits

For which materials and machines

Base materials

Material group: nickel alloys. The exact grades and thicknesses are in the manufacturer data sheet, and for an unusual joint call us, we will pick the filler metal.

current: DC+

Process and machines

Stick electrode, works on any sound machine for this process: welders.

Used welders New welders Ask us to help you choose
Technical substitute

Consumables with the same classification

Same material group, matching classification, a shared diameter and the same shielding gas. Confirm any substitute for your WPS in the documentation.

From the same group

Other consumables for the same material

For comparison before you buy. A technical substitute is listed above.

All: Stick electrodes