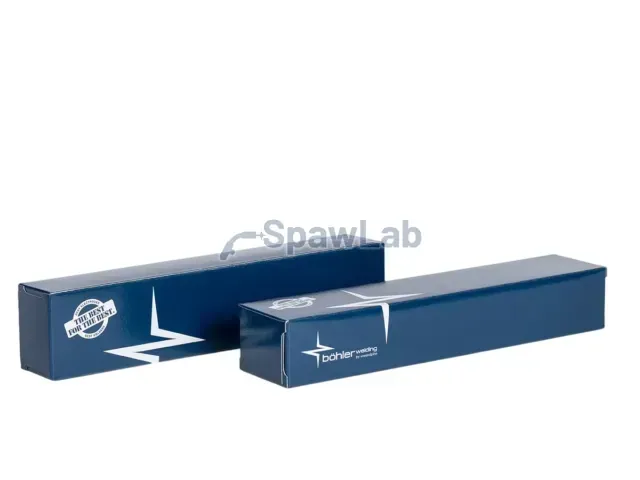
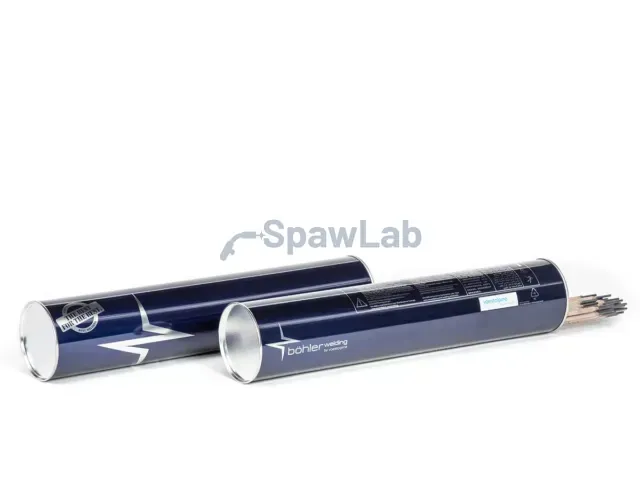
Böhler Welding, stick electrode, creep-resistant CrMo steels

BÖHLER FOX CM 2 Kb stick electrode

EN ISO classificationEN ISO 3580-A: E CrMo2 B 4 2 H5, EN ISO 3580-B: E6218-2C1M H5
AWS classificationAWS A5.5 / SFA-5.5: E9018-B3 H4R, AWS A5.5M: E6218-B3 H4R
ApprovalsTÜV (00722), DB (10.014.81), ABS, DNV, CE
Price on request
Give us the diameter and the quantity, we will quote during working hours

Spawlab is the data controller. We will use your data only for replying to this price enquiry. See the privacy policy for details.

Authorised distributorvoestalpine Böhler Welding
Courier shippingfrom the warehouse in Krotoszyn
Data sheetcomposition, properties, specifications
Wire selectionhelp from a welding engineer
Manufacturer data sheet
Application

What BÖHLER FOX CM 2 Kb stick electrode is used for

BÖHLER FOX CM 2 Kb is a covered electrode with a basic coating for shielded metal arc welding. The 2.25Cr-1Mo type deposit has a bainitic structure and good mechanical properties in the tempered and in the quenched and tempered condition, and under certain conditions service in the as welded condition is possible. The manufacturer directs it to joints in creep resistant steels and cast steels of this class in thermal power and chemical plants.

The base materials are 1.7380 (10CrMo9-10), 1.7375 (12CrMo9-10) and 1.7276 (10CrMo11). The approval covers service under creep conditions at design temperatures up to 600 degrees C. A very low content of trace elements gives a Bruscato factor below 15 ppm, so the deposit resists temper embrittlement and meets the requirements of the step cooling test. From the basic coating the manufacturer obtains about 110 percent metal recovery.

  • Classification EN ISO 3580-A: E CrMo2 B 4 2 H5
  • Classification EN ISO 3580-B: E6218-2C1M H5
  • AWS classification A5.5 / SFA-5.5: E9018-B3 H4R
  • Coating: basic
  • Current: DC+
  • Diameters: 2.5 / 3.2 / 4.0 / 5.0 mm
  • Lengths: 250, 350 and 450 mm
  • Approvals: TÜV (00722), DB (10.014.81), ABS, DNV, CE

Steel of the 2.25Cr-1Mo type is welded with preheating, and the stress relieving after welding is set by the data sheet of the base material. If the design allows service without heat treatment, check that condition in the documents, because it applies only to defined thicknesses and applications. Dry the electrodes to the instructions and take them out of the oven in batches for an hour of work. On heavy vessel walls spread the filling over many thin layers.
Manufacturer datasheet

Chemical composition and properties from the manufacturer datasheet

Datasheet PDF

Typical weld metal values from the voestalpine Böhler Welding data sheet, issue 06/2025. The minimum or the range guaranteed by the maker is given in brackets. The figures depend on the heat treatment condition and the shielding gas stated in the row and do not replace testing the joint to your own WPS.

Welding data and approvals
Polaritydirect current, electrode positive (DC+)
ApprovalsTÜV (00722), DB (10.014.81), ABS, DNV, CE
Datasheet edition06/2025
Fits

For which materials and machines

Base materials
  • 1.7380
  • 10CrMo9-10
  • 1.7375
  • 12CrMo9-10
  • 1.7276
  • 10CrMo11

current: DC+

Process and machines

Stick electrode, works on any sound machine for this process: welders.

Used welders New welders Ask us to help you choose
Technical substitute

Consumables with the same classification

Same material group, matching classification, a shared diameter and the same shielding gas. Confirm any substitute for your WPS in the documentation.

From the same group

Other consumables for the same material

For comparison before you buy. A technical substitute is listed above.

All: Stick electrodes