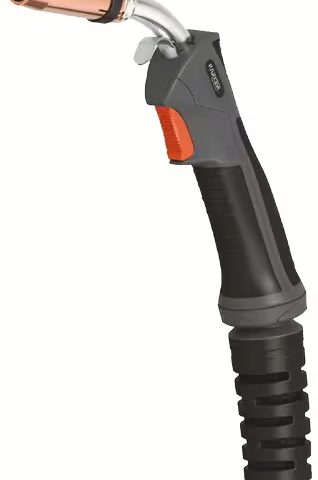


The Kemppi FastMig Pulse 350 is a used MIG/MAG welder with pulse and double pulse and with purchased licences for WiseFusion and WisePenetration, the Kemppi software that keeps the arc length and current under control when the wire stick-out changes. It has programs for steel, aluminium and stainless steel, and delivers 350 A at 80% and 330 A at 100% duty cycle. The set includes the MXF 65 wire feeder with PF 65 panel, a FastCool 10 cooling unit, a trolley, a 4 m MIG torch, a 4 m earth cable and a 1.5 m interconnection cable.
- WiseFusion. In pulse and spray arc the arc is held at the short-circuit boundary, so it stays short and focused without constant readjustment of the settings. In a Kemppi test WiseFusion lowered the heat input compared with conventional pulse, and we give the results in the process description.
- WisePenetration. The current does not drop with a long wire stick-out: in the Kemppi example, at 30 mm it stays at 280 A instead of 240 A.
- Pulse and double pulse. Almost spatter-free transfer on aluminium and stainless steel and a weld face with regular ripples.
- Premium class of its time. Kemppi wrote that the FastMig Pulse leads its class in welding quality, and aimed it at shipyards, offshore, the chemical industry and welded fabrication.
- MXF 65 wire feeder with DuraTorque 400 drive. Four rolls, a metal door on the spool compartment, stable feeding of aluminium and cored wire.
- 100 memory channels with access control. 10 users with 10 channels each, PIN lock and channel lock from the wire feeder panel.
Welding processes of the Kemppi FastMig Pulse 350
Pulse and 1-MIG synergic control
In 1-MIG you choose a program for the material, wire, diameter and gas, and then you adjust only the wire speed. The curve sets the voltage, and you correct the arc length from -9.0 to +9.0. In pulse the current switches between the base current and a pulse that detaches the droplet without a short circuit. On stainless steel and aluminium this gives almost spatter-free transfer, a smooth weld face and welding in all positions. You correct the pulse current from -10 to +15% relative to the program.
Double pulse: weld pool rhythm and a rippled weld face
On top of normal pulse the machine superimposes a slow modulation of the wire speed, and the pulse parameters follow it along the curve. The arc alternates between a hotter and a cooler phase: you set the frequency from 0.4 to 8.0 Hz and the amplitude of the wire speed change from 0.1 to 3.0 m/min. Each cycle leaves one ripple, so the ripple spacing is roughly the travel speed divided by the frequency: at 40 cm/min and 2 Hz about 3.3 mm.
Double pulse is not a way to weld cold. Its strength is weld pool control: positional welding is easier, you keep the gap under control and get a regular weld face that on aluminium and stainless steel resembles TIG. You have double pulse in the programs marked Pulse/Double Pulse, including those for aluminium and stainless steel, and WiseFusion works together with it.
WiseFusion: the arc kept short as if on cruise control
In pulse and in spray arc the arc tends to get longer when the wire stick-out or the torch position changes. WiseFusion counts short circuits and regulates the arc length so that a set share of droplets touches the weld pool before detaching. The arc stays at the short-circuit boundary, like a car with adaptive cruise control that keeps a constant distance from the car in front by itself. The WiseFusion setting from 10 to 60% is exactly this share of droplets passing through a short circuit, not a percentage of power. The default is 50% for aluminium and 35% for steel.
The result: a short, focused arc, a smaller weld pool and easier positional welding, especially vertical welding of aluminium. In a Kemppi test at a wire speed of 12 m/min and a travel speed of 450 mm/min, heat input (arc energy) was 0.59 kJ/mm with WiseFusion, 0.68 kJ/mm with conventional pulse and 0.80 kJ/mm with conventional MAG. Lappeenranta University of Technology (LUT), working with the Arctech Helsinki shipyard, showed that WiseFusion and WisePenetration make it possible to reduce the groove angle from 45 to 30 degrees, which means less filler metal in every joint.
WisePenetration: current that does not drop with long stick-out
In conventional MIG/MAG a longer wire stick-out lowers the current, and with it the penetration, although the voltage and wire speed on the display do not change. WisePenetration works like a threshold: as long as the stick-out is within the normal range, the arc works as usual, and when it grows beyond the setting, the machine speeds up the wire and does not let the current drop. In the Kemppi example, with a stick-out of 30 mm the current stays at 280 A instead of falling to 240 A.
It helps in the root of fillet welds, in deep grooves and wherever access does not let you keep a constant torch distance: less lack of fusion and incomplete penetration, less grinding and repair. You set the correction from -30 to +30%. In this generation WisePenetration works in 1-MIG synergic programs for steel, not in pulse and not in the programs for aluminium and stainless steel.
Manual MIG/MAG
You set the voltage from 8.0 to 50.0 V in 0.1 V steps and the wire speed separately when you weld with a wire or gas for which the machine has no curve.
Functions and settings
- Hot Start from -50 to +100%, time in 2T from 0.0 to 9.9 s. Extra energy at the start of the weld, so that cold, thick aluminium fuses straight away.
- Crater fill from 10 to 250% over a time from 0.0 to 10.0 s. At the end of the weld the current goes down gradually, so the risk of crater cracks is lower.
- Slow wire start from 10 to 99% and ignition correction from -9 to +9. Soft, clean ignition without the wire bouncing back.
- Cable length compensation from 10 to 100 m. The arc behaves the same with a short or a long interconnection cable.
- Control from the PF 65 panel. You change power and arc length at the wire feeder, also during welding. Gas test and wire inching are on the same panel.
- Up to 4 wire feeders on one source. If you add a second wire feeder, you can have, for example, steel wire and aluminium wire set up separately without reconfiguring.
- FastCool 10 cooling unit. 1 kW capacity, tank of about 3 l, TEST button and coolant circuit monitoring.
How the Kemppi FastMig Pulse 350 compares with the competition
Other major brands have equivalents of the Wise functions: Fronius has the Penetration Stabilizer and Arc Length Stabilizer in the TPS/i, EWM has wiredArc and forceArc, and double pulse appears as SynchroPulse at Fronius, superPuls at EWM, SuperPulse at ESAB, Pulse-on-Pulse at Lincoln and DUO Plus at Migatronic.
Kemppi documentation described WiseFusion and WisePenetration in the FastMig Pulse as early as 2011. In this unit you get WiseFusion, WisePenetration and double pulse in a machine that Kemppi positioned in the premium class.
Technical data
| Manufacturer | Kemppi Oy, Lahti, Finland |
|---|---|
| Model | FastMig Pulse 350, P65 panel, MXF 65 wire feeder with PF 65 panel (also written as: FastMig Pulse350, Kemppi Pulse 350) |
| Type | inverter MIG/MAG welder with synergic control, pulse and double pulse |
| Mains supply | 3 x 400 V, from -15 to +20%, 50/60 Hz |
| Mains fuse | 25 A time-delay |
| Duty cycle 40°C | 350 A at 80%, 330 A at 100% |
| Mains power | 16.0 kVA at 80%, 15.3 kVA at 100% |
| Open circuit voltage | 80 V |
| Efficiency and power factor | 88% and 0.85 |
| IP rating | IP23S |
| Purchased functions | WiseFusion, WisePenetration, double pulse |
| Double pulse | from 0.4 to 8.0 Hz, wire amplitude from 0.1 to 3.0 m/min |
| WiseFusion and WisePenetration | from 10 to 60% and from -30 to +30% |
| Memory | 100 MIG channels (10 x 10) |
| Source dimensions (L x W x H) | 590 x 230 x 430 mm |
| Source weight | 36 kg |
| MXF 65 wire feeder | DuraTorque 400, 4 rolls, from 0 to 25 m/min, spool up to 20 kg |
| Wire diameters | steel from 0.6 to 1.6 mm, cored from 0.8 to 2.0 mm, aluminium from 1.0 to 2.4 mm |
| Cooling unit | FastCool 10, 1 kW, about 3 l |
What you get
- Kemppi FastMig Pulse 350 power source with P65 panel
- MXF 65 wire feeder with PF 65 panel
- FastCool 10 cooling unit
- trolley
- MIG torch, 4 m long
- earth cable, 4 m long
- interconnection cable, 1.5 m long
What to watch out for
The source needs a 3 x 400 V connection with a 25 A time-delay fuse. MMA, WiseRoot, WiseThin and MatchLog are separate licences on this platform, and this unit does not have them. Before you buy, we will send you a photo of the program list from the menu, with wire diameters and gases. The housings have signs of use visible in the photos.
Questions about the Kemppi FastMig Pulse 350
Is the Kemppi FastMig Pulse 350 suitable for aluminium?
Yes. It has aluminium programs with pulse and double pulse, WiseFusion with a default setting of 50% for aluminium, and the four-roll DuraTorque 400 wire feeder.
Do you have to buy the Wise functions separately?
No. WiseFusion, WisePenetration and double pulse are purchased and permanently activated on this unit. It does not, however, have MMA, WiseRoot, WiseThin or MatchLog.
What does WiseFusion do in practice?
A short, focused arc without constant correction of the arc length, a smaller weld pool and easier positional welding. In a Kemppi test the heat input was lower than with conventional pulse and with conventional MAG.
Does WisePenetration work in pulse?
No. In this generation it works in 1-MIG synergic programs for steel. The newer WisePenetration+ version works with pulse (for example in the Kemppi X8).
What power connection do I need?
3 x 400 V with a 25 A time-delay fuse.
How we sell used machines
Unit checked in our service centre in Krotoszyn, with measurements to PN-EN 60974-4 and a load test. The price includes the first year of the service package: cleaning, basic inspection and electrical measurements. The measurement report is part of the paid service package. You can buy further years. We ship across the European Union, personal collection by appointment.