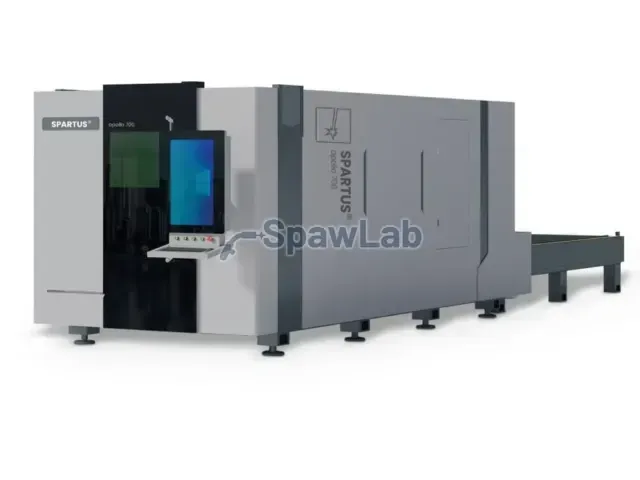
SPARTUS APOLLO 500 LASER CUTTING MACHINE: CUTTING PRECISION FOR MODERN PRODUCTION
CONCENTRATED POWER AND HIGH QUALITY
The SPARTUS Apollo 500 is a modern fibre laser cutting machine with an output of 3 kW, built for precise sheet metal cutting. The integrated Raycus laser source and the Raytools BM110 cutting head with autofocus deliver not only
excellent cut quality, but also a long service life and stable operation even in intensive
production use.
COMPACT AND STABLE DESIGN
The Apollo 500 is built on a reinforced welded frame machined to tight tolerances. The gantry design with rack-and-pinion drive gives rigidity, resistance to vibration and excellent dynamics. The cross beam, made of cast aerospace-grade aluminium, resists deformation and has a long service life.
EFFECTIVE DUST EXTRACTION AND ENCLOSED HOUSING
The machine is fully enclosed, and the extraction is divided into zones: air is blown in on one side and extracted on the other. This layout removes smoke and dust directly from the cutting area, keeping it clean and safe and protecting the optical components.
ADVANCED OPTICS FOR DEMANDING APPLICATIONS
Raytools BM110 is a cutting head designed for heavy-duty use: it has autofocus, advanced lens cooling and four protective windows.
INTUITIVE OPERATION AND FULL CONTROL
Raytools X3S , an industrial-grade control system, offers full CAD/CAM/NEST integration. It automatically corrects errors in drawings, optimises the cutting path and supports advanced production planning. The 21-inch screen gives you quick access to all functions, and the built-in statistics and motion error compensation ensure repeatable results.
VOLTAGE STABILISER, SAFETY AND RELIABLE POWER SUPPLY
The SPARTUS Apollo 500 is equipped with a 40 kVA voltage stabiliser, which plays a key role in keeping the machine running safely and steadily. It automatically adapts the supply parameters to local grid conditions, whatever the country or region. Voltage stabilisation and regulation protect the electronics against surges and interference, which extends component life and makes the whole laser system more reliable.
ENGINEERING DETAILS AND PRACTICAL FEATURES
The Apollo 500 is designed to make operation as simple as possible: the work table slides out to the side for easy loading and unloading, and built-in automatic lubrication and camera monitoring help keep production running without interruptions. Electrical components (Schneider Electric), PEK linear guides and Atlanta pinions as well as Leitesen gear racks provide high durability and reliability.
SAMPLES OF PERFECT CUTS
The Apollo 500 handles thin-walled parts, sharp corners and micro-holes with ease and leaves bright, clean edges. It is a machine for demanding industrial work, where speed matters, but quality matters most.
SPARTUS APOLLO 500 CUTTING PARAMETERS
| Material | Thickness [mm] | Cutting speed [m/min] | Laser power [W] | Gas | Pressure [bar] | Nozzle [mm] | Focus position [mm] | Cutting height [mm] |
|---|---|---|---|---|---|---|---|---|
| Carbon steel | 1 | 28-35 | 3000 | N₂/air | 10 | 1.5S | 0 | 1 |
| Carbon steel | 2 | 16-20 | 3000 |
N₂/air |
10 | 2.0S | 0 | 0.5 |
| Carbon steel | 2 | 3.8-4.2 | 2100 | O₂ | 1.6 | 1.0D | +3 | 0.8 |
| Carbon steel | 3 | 3.2-3.6 | 2100 |
O₂ |
0.6 | 1.0D | +4 | 0.8 |
| Carbon steel | 4 | 3-3.2 | 2400 |
O₂ |
0.6 | 1.0D | +4 | 0.8 |
| Carbon steel | 5 | 2.7-3 | 3000 |
O₂ |
0.6 | 1.2D | +4 | 0.8 |
| Carbon steel | 6 | 2.2-2.5 | 3000 |
O₂ |
0.6 | 1.2D | +4 | 0.8 |
| Carbon steel | 8 | 1.8-2.2 | 3000 |
O₂ |
0.6 | 1.2D | +4 | 0.8 |
| Carbon steel | 10 | 1-1.3 | 3000 |
O₂ |
0.6 | 1.2D | +4 | 0.8 |
| Carbon steel | 12 | 0.9-1 | 2400 |
O₂ |
0.6 | 3.0D | +4 | 0.8 |
| Carbon steel | 14 | 0.8-0.9 | 2400 |
O₂ |
0.6 | 3.0D | +4 | 0.8 |
| Carbon steel | 16 | 0.6-0.7 | 2400 |
O₂ |
0.6 | 3.5D | +4 | 0.8 |
| Carbon steel | 18 | 0.5-0.6 | 2400 |
O₂ |
0.6 | 4.0D | +4 | 0.8 |
| Carbon steel | 20 | 0.4-0.55 | 2400 |
O₂ |
0.6 | 4.0D | +4 | 0.8 |
| Carbon steel | 22 | 0.45-0.5 | 2400 |
O₂ |
0.6 | 4.0D | +4 | 0.8 |
| Stainless steel | 1 | 28-35 | 3000 | N₂ | 10 | 1.5S | 0 | 0.8 |
| Stainless steel | 2 | 18-24 | 3000 |
N₂ |
12 | 2.0S | 0 | 0.5 |
| Stainless steel | 3 | 7-10 | 3000 |
N₂ |
12 | 2.5S | -0.5 | 0.5 |
| Stainless steel | 4 | 5-6.5 | 3000 |
N₂ |
14 | 2.5S | -1.5 | 0.5 |
| Stainless steel | 5 | 3-3.6 | 3000 |
N₂ |
14 | 3.0S | -2.5 | 0.5 |
| Stainless steel | 6 | 2-2.7 | 3000 |
N₂ |
14 | 3.0S | -3 | 0.5 |
| Stainless steel | 8 | 1-1.2 | 3000 |
N₂ |
16 | 3.5S | -4.5 | 0.5 |
| Stainless steel | 10 | 0.5-0.6 | 3000 |
N₂ |
16 | 4.0S | -6 | 0.5 |
| Aluminium | 1 | 25-30 | 3000 | N₂ | 12 | 1.5S | 0 | 0.8 |
| Aluminium | 2 | 15-18 | 3000 |
N₂ |
12 | 2.0S | 0 | 0.5 |
| Aluminium | 3 | 7-8 | 3000 |
N₂ |
14 | 2.0S | -1 | 0.5 |
| Aluminium | 4 | 5-6 | 3000 |
N₂ |
14 | 2.5S | -2 | 0.5 |
| Aluminium | 5 | 2.5-3 | 3000 |
N₂ |
16 | 3.0S | -3 | 0.5 |
| Aluminium | 6 | 1.5-2 | 3000 |
N₂ |
16 | 3.0S | -3.5 | 0.5 |
| Aluminium | 8 | 0.6-0.7 | 3000 |
N₂ |
16 | 3.5S | -4 | 0.5 |
Note: The parameters marked in red in the table apply to test production only and are not recommended for series production. For thicker materials, a laser with a higher output is recommended.