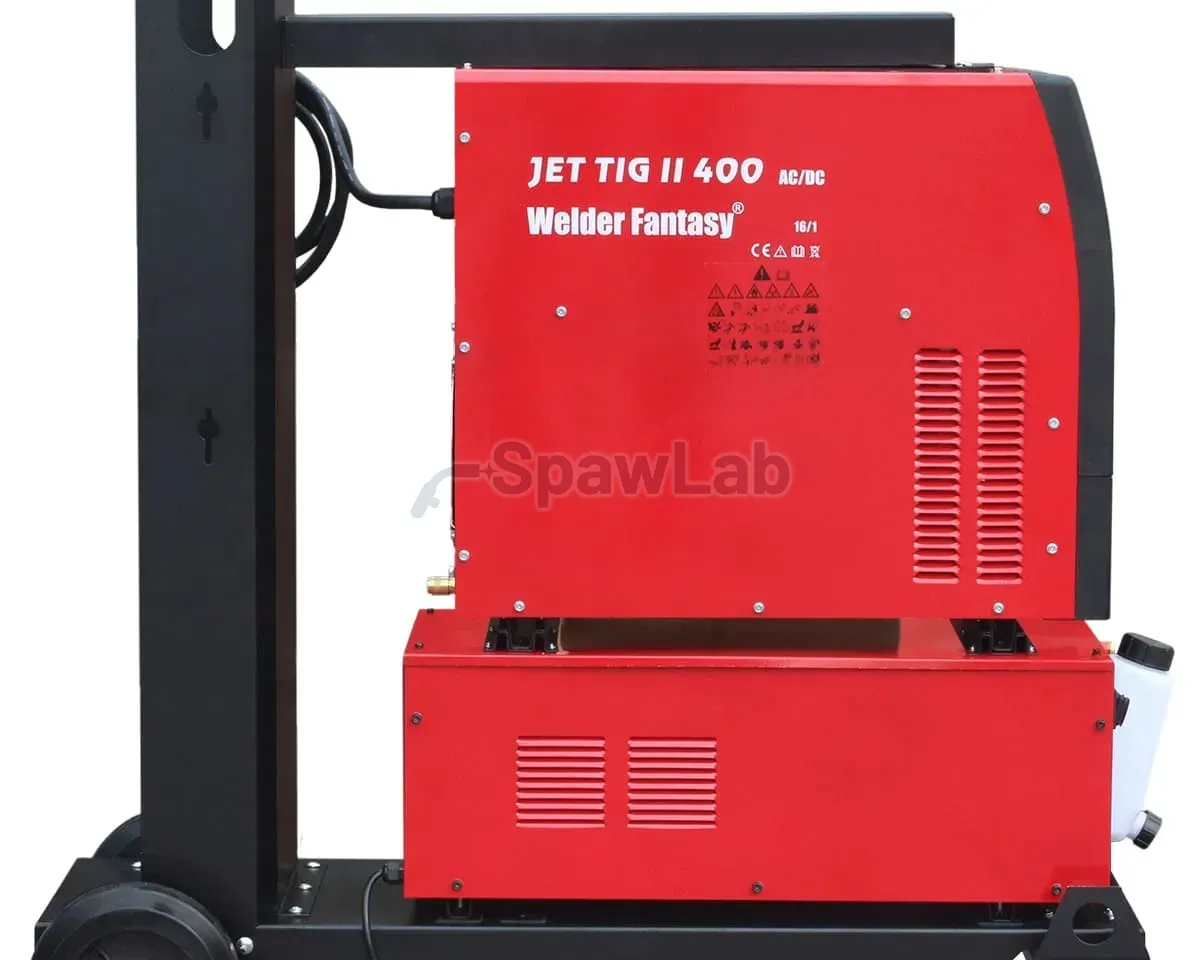
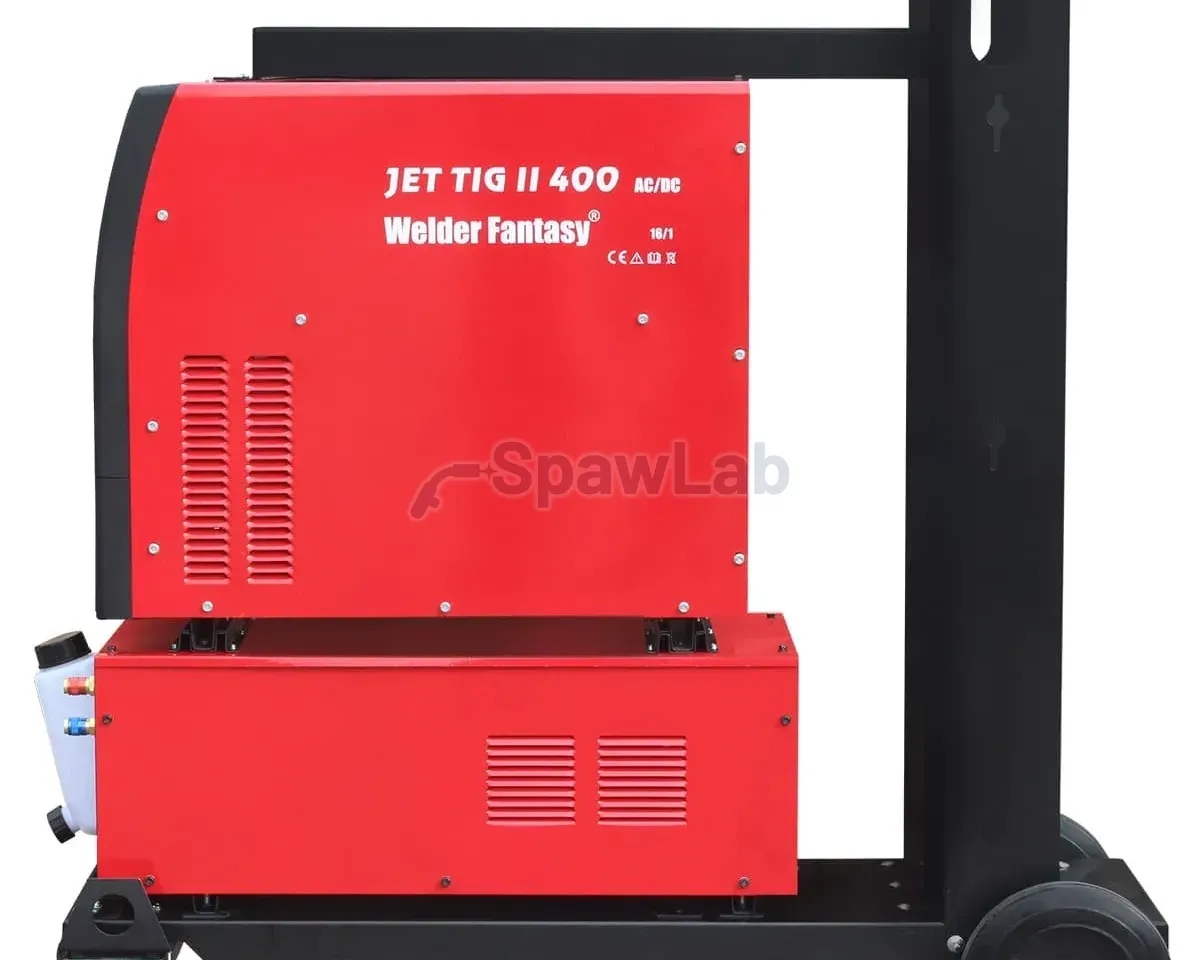
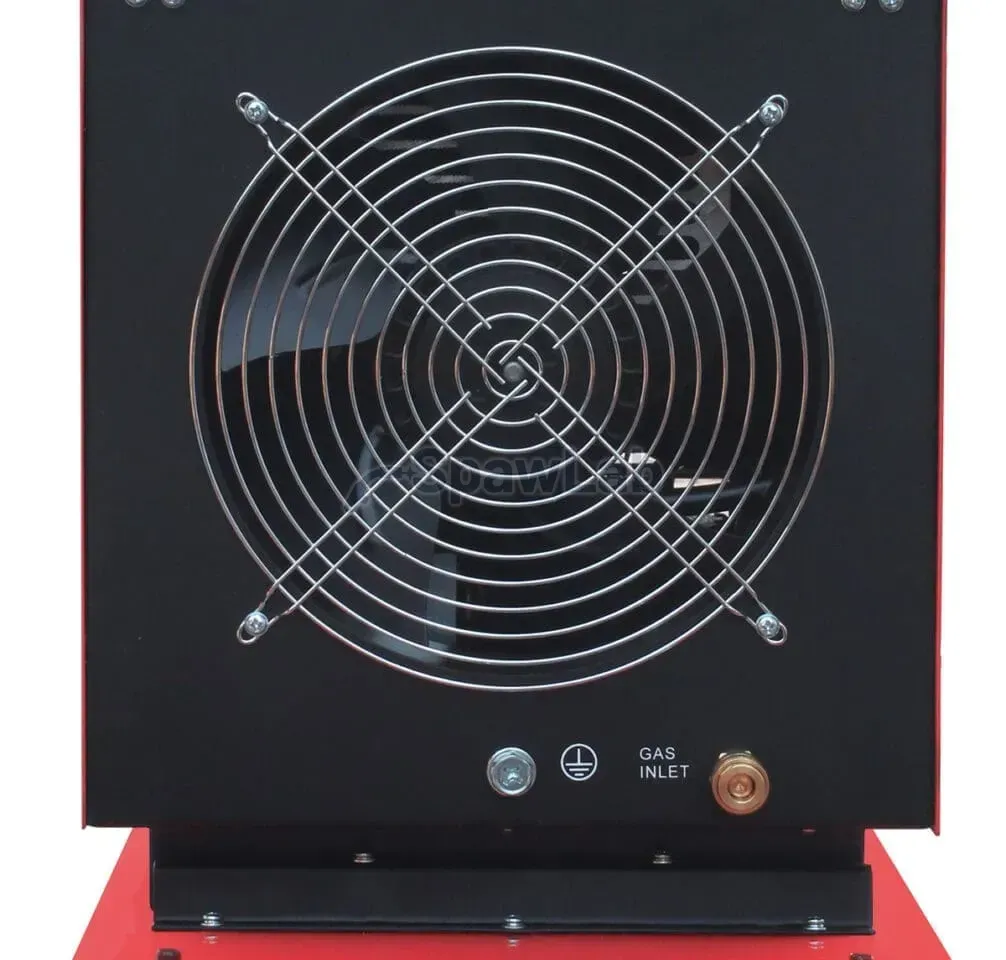


Welder Fantasy is a brand created by the company FACHOWIEC in 1991. Inverter TIG/MMA welders, MIG/MAG welders, plasma cutters and the other equipment carrying the Welder Fantasy mark have been chosen for years by thousands of workshops and companies in Poland and abroad. The Welder Fantasy brand means:
- Top quality of the machines,
- Guaranteed reliability,
- High working parameters,
- Leader on the Polish market.
The most advanced TIG machine on the Polish market. Functions that were out of reach until now are available today.
Technology: IGBT - Insulated Gate Bipolar Transistor - is a modern technology based on bipolar transistors with an insulated gate. It combines the easy control of field-effect transistors with the high breakdown voltage and the switching speed of bipolar transistors. IGBT technology considerably extends the reliable service life of welding machines.
High efficiency of the machine 60%.
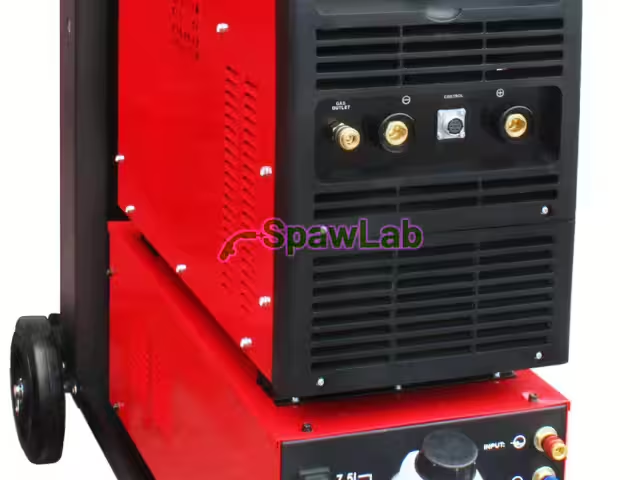
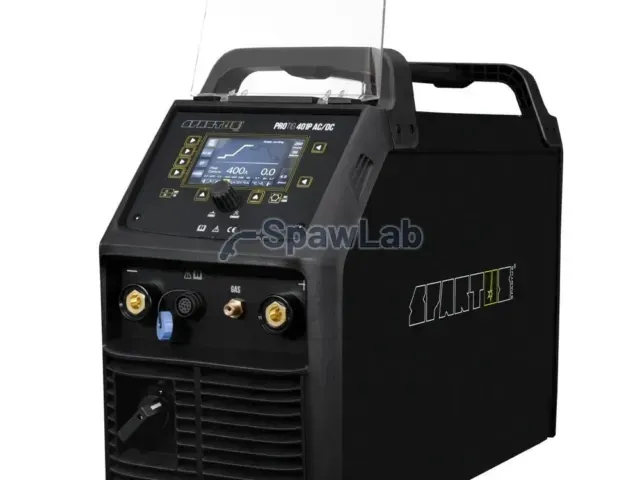
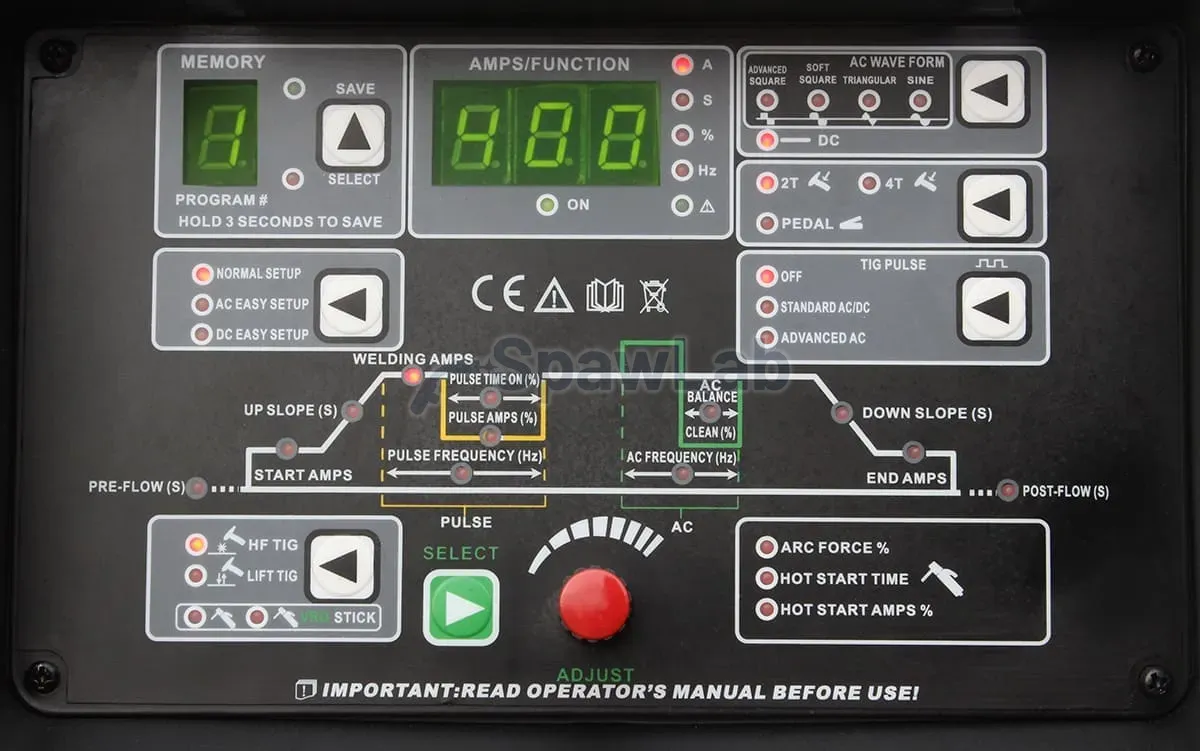
This top class machine sets new standards among AC/DC welding machines, and the clear control panel gives access to every working parameter you need. The standard equipment includes TIG ARC T5W 8M. -> technical data
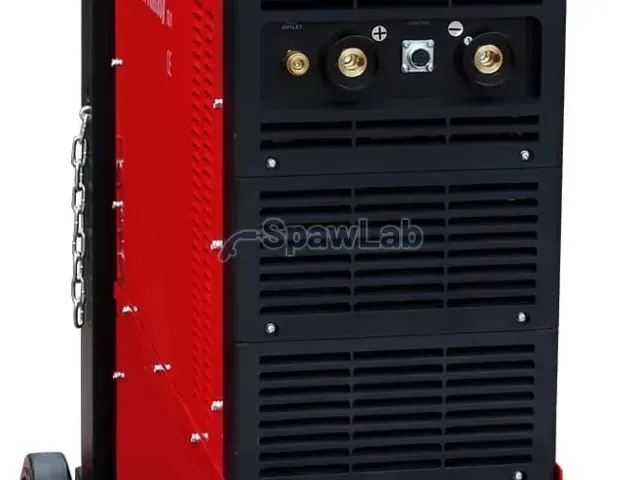
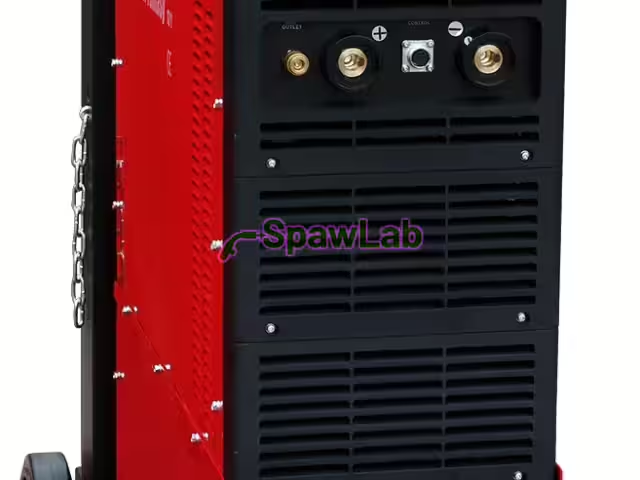
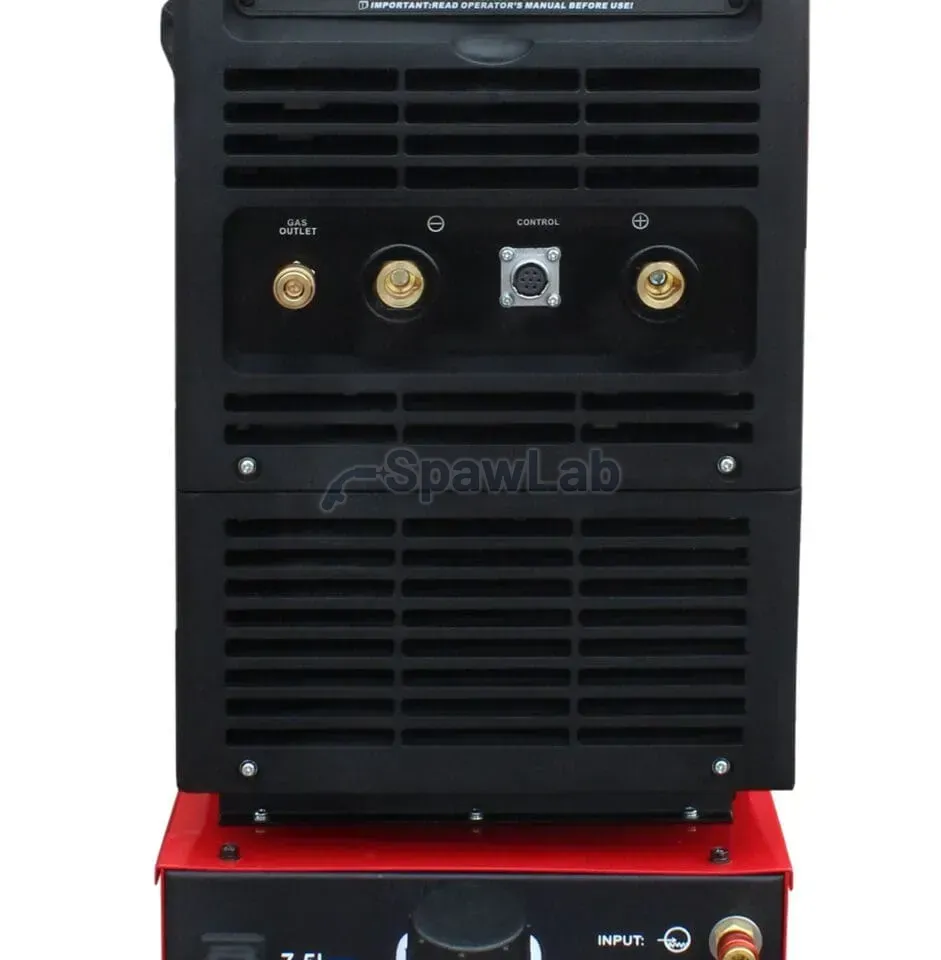
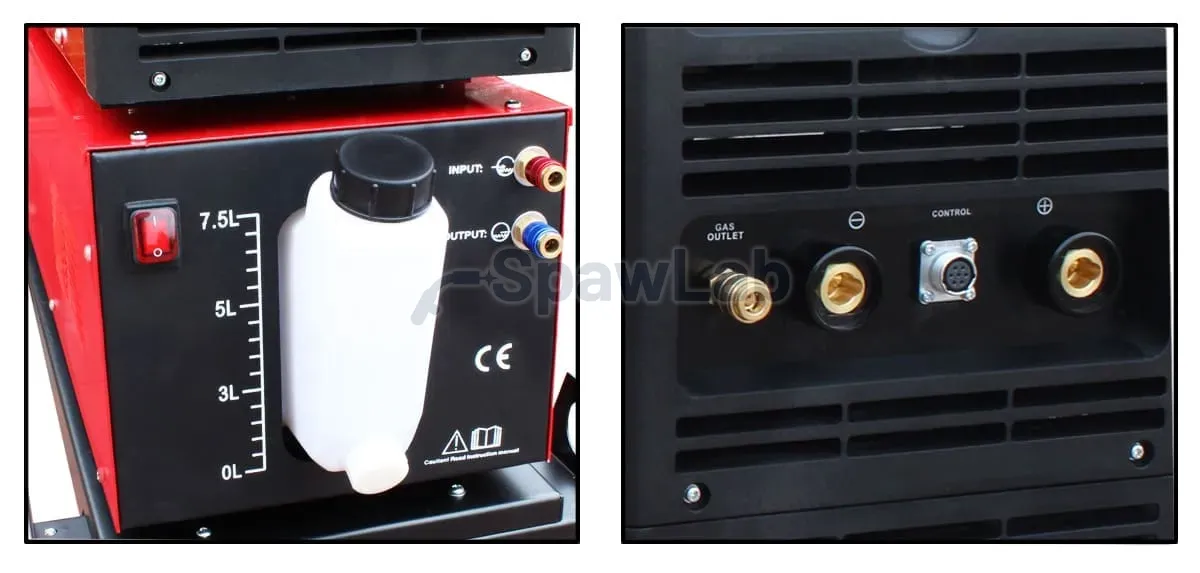
The industrial machines Welder Fantasy JET TIG II AC/DC 400 are microprocessor welding power sources based on IGBT technology, fitted with a water-cooled torch and a cooling unit, suited to welding carbon steels, stainless and acid-resistant steels, copper, brass, magnesium, titanium and all aluminium alloys.
MACHINE FEATURES:
- compact build,
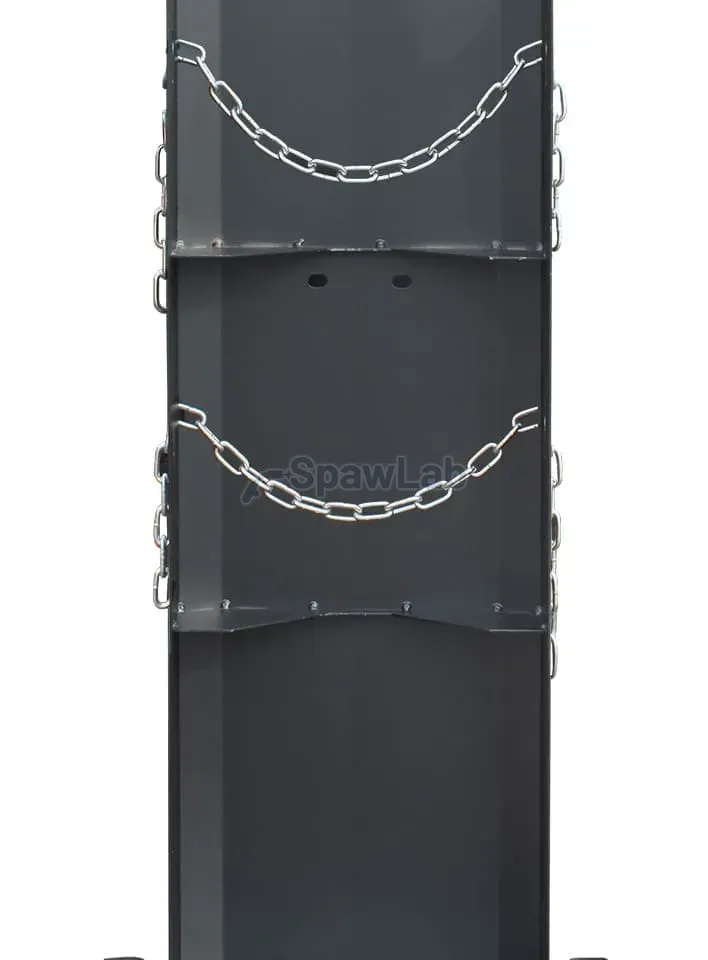
- integrated design with cooling unit and trolley,
- transistors: IGBT,
- efficiency 60%,
- control panel that is easy to operate,
- LCD display of the welding parameters,
- LCD display of the individual program,
- option to store a full 9 user programs,
- a very broad choice of welding functions.
The machine welds with the following methods:
TIG DC lift-arc - In the TIG method (Tungsten Inert Gas) the arc is struck under a shield of inert gas (argon), between the workpiece and a non-consumable electrode made of pure tungsten or tungsten with additives. In TIG lift-arc mode the arc is struck the moment the electrode touches the workpiece. In TIG DC mode the current is constant.
TIG DC HF - To rule out any contamination of the weld with tungsten, the electrode should not touch the workpiece; for that reason the arc is struck without contact, using high frequency discharges produced by the ionizer built into the machine.
TIG DC PULS lift-arc - the arc is struck by contact between the electrode and the workpiece, the pulse function allows thin parts to be welded through periodic changes of the current.
TIG DC PULS HF - contactless HF striking with the ionizer in TIG DC PULS mode
TIG AC lift-arc - a function for welding aluminium with alternating current, which during aluminium welding provides cathodic cleaning. The AC BALANCE parameter, the balance of the alternating current, sets the ratio between the durations of its phases.
TIG AC HF - the same function for welding aluminium with alternating current, the arc is struck without contact by high frequency current from the ionizer
TIG AC PULS lift-arc - welding in this mode combines alternating current with pulse, which allows very thin aluminium parts to be welded. The arc is struck by contact between the electrode and the workpiece.
TIG AC PULS HF - a function for welding aluminium parts of small thickness. Contactless striking thanks to the ionizer.
TIG AC + DC - the ADVANCED AC function allows welding with mixed current AC DC- In a single cycle the machine passes between alternating current AC and direct current of negative polarity DC(-). That cycle repeats through the whole welding process. Welding with mixed current is particularly useful when joining parts of different thickness. Noise emission is also lower than with AC welding.
MMA DC+ - The MMA method uses a covered electrode made of a metal core with a coating. An arc forms between the tip of the electrode and the workpiece. The arc is struck by touching the workpiece with the tip of the electrode. MMA DC+ means welding with positive polarity, more heat goes into the material and less into the electrode.
MMA DC- - the difference from MMA DC+ is that the polarity in MMA DC - mode is negative, so the heat distribution is reversed, more heat goes into the electrode and less into the workpiece.
MMA VRD DC+ - the VRD function available in MMA DC+ mode ( Voltage Reduction Device, a module that reduces the open circuit voltage of the secondary circuit of the machine. It raises safety and limits the risk of electric shock. The function switches the welding supply off and on when resistance is measured between the electrode and workpiece terminals during welding.
MMA VRD DC- - the VRD function available in MMA DC- mode ( Voltage Reduction Device) works in the same way as MMA VRD DC+, the difference lies in the negative polarity.
PANEL FUNCTIONS:
- Option to use the factory settings programmed by the user for welding aluminium and steel (9 memory channels)
- Option to choose the waveform:
ADVANCED SQUARE - the rectangular waveform of the alternating current allows welding of aluminium with magnesium content
SOFT SQUARE - the trapezoidal waveform of the alternating current is used for welding aluminium with silicon content
TRIANGULAR - the triangular current waveform is best for welding thin parts, including anodized aluminium
SINE - the sine waveform is recommended for welding pure aluminium 99.999%
- AC/DC EASY SETUP - option to use the preset factory settings.
- NORMAL SETUP - welding parameters set to individual needs.
- HOT START - a function that raises the current as the arc is struck and makes starting the weld easier.
- ARC FORCE - short circuit current control - as the arc gets shorter the welding current rises, which keeps the arc stable whatever the variation in length.
- HF - the machine carries an ionizer that strikes the welding arc without contact.
- PRE and POST GAS - gas flow before and after welding.
- UP and DOWN SLOPE - rise and fall of the welding current.
- PULSE - welding mode with pulsed current.
- VRD - Voltage Reduction Device - reduces the open circuit voltage of the secondary circuit of the machine. It raises safety and limits the risk of electric shock.
- PFC - Power Factor Correction - raises the power factor as close as possible to 100% in order to cut power losses in the supply lines.
- 2-STROKE and 4-STROKE,
- contactless striking with HF and by scratch start LIFT,
- option to connect remote control - a control pedal, a torch with a potentiometer,
- two-function knob ADJUST (coarse and fine adjustment),
- and others, described in the operating manual.
TECHNICAL DATA:
|
Supply voltage |
3~400V 50 Hz |
|
TIG DC welding current range |
5-400 A |
|
TIG AC welding current range |
10-400 A |
|
TIG efficiency |
400A-35% |
|
Waveform |
rectangular, trapezoidal, triangular, sine |
|
AC current frequency adjustment |
20-250 Hz |
|
Current balance in AC mode |
5%-90% |
|
Pre-gas / post-gas AC/DC mode |
0-25 / 0-50 s |
|
Start / end current DC mode |
5-400 A |
|
Start / end current AC mode |
10-400 A |
|
Slope up / slope down time AC/DC mode |
0-25 s / 0-25 s |
|
Pulse base AC/DC |
3-100% |
|
Pulse duration AC/DC |
5%-95% |
|
Mixed current frequency Advanced AC |
0.1-10 Hz |
|
Pulsed current frequency Standard DC |
0.1-500 Hz |
|
Pulsed current frequency Standard AC Square (rectangular) |
0.1-250 Hz |
|
Pulsed current frequency Standard AC Soft Square, Triangular, Sine |
0.1-10 Hz |
|
TIG arc striking function |
HF (ionizer) / LIFT |
|
Open circuit voltage MMA / VRD MMA |
70 / 21 V |
|
MMA welding current range DC+ / DC- |
20-315 A |
|
MMA efficiency |
315A-60% |
|
ARC FORCE |
0-100% |
|
HOT START TIME |
0-2 s |
|
HOT START AMPS |
0-100% |
|
Power draw TIG/MMA |
11.5 kVA |
|
Slow blow fuse MIN |
32 A |
| Weight | 54kg |
| Set dimensions (L/H/W) | 1060 x 1155 x 435 mm |
All TIG methods can be run in the following welding modes:
- Through the LIFT-ARC system (2T and 4T)
- Contactless HF striking (2T and 4T)
- With the remote control pedal (2T and 4T)
THE COMPLETE SET CONTAINS:
- the welder Welder Fantasy JET TIG II AC/DC 400 IGBT,
- cooling unit filled with welding coolant,
- integrated transport trolley,
- water-cooled welding torch - torch TIG ARC T5W 8M -> technical data
- earth clamp 3m,
- electrode holder 3m,
- operating manual and warranty card.
“WELDER FANTASY” IS A PROTECTED AND REGISTERED TRADEMARK - see the Protection Certificate document