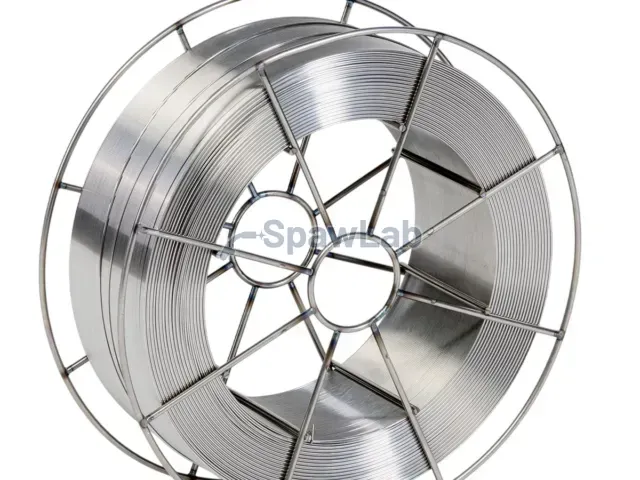
Böhler Welding, flux-cored wire, stainless and acid-resistant steels

FOXcore 308 H-T1 flux-cored wire

EN ISO classification17633-A T Z 19 9 H P M21 (C1) 1
AWS classificationA5.22 / SFA-5.22 E308HT1-4(1)
Shielding gasC1: 100 % CO2, M21: Ar with 15 to 25 % CO2
ApprovalsTÜV (11151), CE
Price on request
Give us the diameter and the quantity, we will quote during working hours

Spawlab is the data controller. We will use your data only for replying to this price enquiry. See the privacy policy for details.

Authorised distributorvoestalpine Böhler Welding
Courier shippingfrom the warehouse in Krotoszyn
Data sheetcomposition, properties, specifications
Wire selectionhelp from a welding engineer
Manufacturer data sheet
Application

What FOXcore 308 H-T1 flux-cored wire is used for

FOXcore 308 H-T1 is a high-alloyed flux-cored wire of the E 308 type for creep resistant austenitic stainless steel, suitable for all welding positions and run under a mixed shielding gas.

It joins grades such as 1.4301, X5CrNi18-10, 1.4541, 1.4550, 1.4878, 1.4948 and X7CrNi18-9 together with their equivalents. All positions are open to it, the composition protects the joint against intergranular corrosion, and the austenitic deposit holds up against creep at elevated temperature.

  • Classification EN ISO: 17633-A T Z 19 9 H P M21 (C1) 1
  • AWS classification: A5.22 / SFA-5.22 E308HT1-4(1)
  • Shielding gas: M21, C1
  • Diameters: 1.2 / 2.0 mm
  • Approvals: TÜV (11151), CE

After welding remove the heat tint by pickling or brushing, the oxide layer alone lowers the corrosion resistance of the joint. Store the wire dry and do not leave an open spool in the feeder overnight, the core takes up moisture.
Manufacturer datasheet

Chemical composition and properties from the manufacturer datasheet

Datasheet PDF

Typical weld metal values from the voestalpine Böhler Welding data sheet, issue 01/2021. The minimum or the range guaranteed by the maker is given in brackets. The figures depend on the heat treatment condition and the shielding gas stated in the row and do not replace testing the joint to your own WPS.

Welding data and approvals
Polaritydirect current, electrode positive (DC+)
Shielding gas to EN ISO 14175M2
ApprovalsTÜV (11151), CE
Datasheet edition01/2021
Mechanical properties of the all-weld metal, typical values
Condition Yield strength Re, MPa Tensile strength Rm, MPa Elongation A, % Impact energy KV, J at 20 °C
u 370 (min. 350) 560 (min. 550) 45 (min. 30) 90 (min. 32)
  • u: untreated, as-welded, shielding gas M21 (Ar + 18% CO2 )
Fits

For which materials and machines

Base materials
  • 1.4301
  • X5CrNi18-10
  • 1.4541
  • 1.4550
  • 1.4878
  • 1.4948
  • X7CrNi18-9
  • UNS S30400
  • AISI 304
  • 304H
  • 321H
  • 347H
Process and machines

Flux-cored wire, works on any sound machine for this process: welders. Shielding gas: C1: 100 % CO2, M21: Ar with 15 to 25 % CO2.

Used welders New welders Ask us to help you choose
Technical substitute

A substitute for this consumable

We will find a substitute with the same classification, diameter and shielding gas over the phone: +48 669 162 833.

From the same group

Other consumables for the same material

For comparison before you buy. A technical substitute is listed above.

All: Flux-cored wires