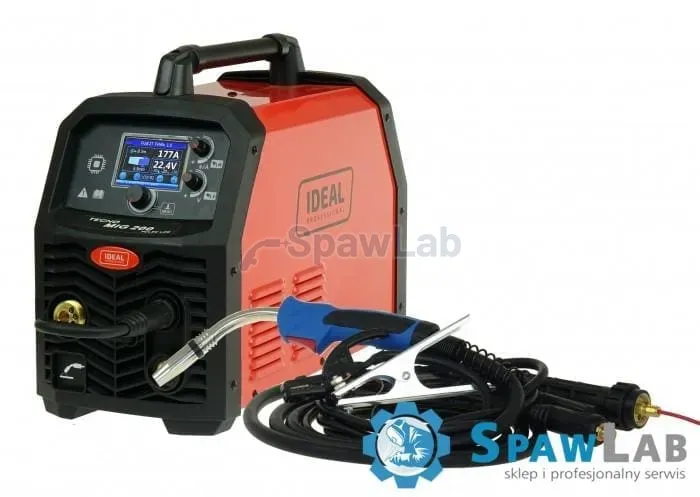
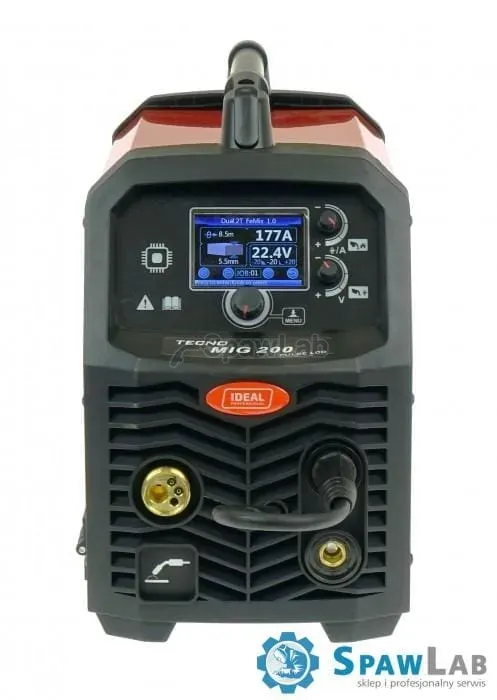
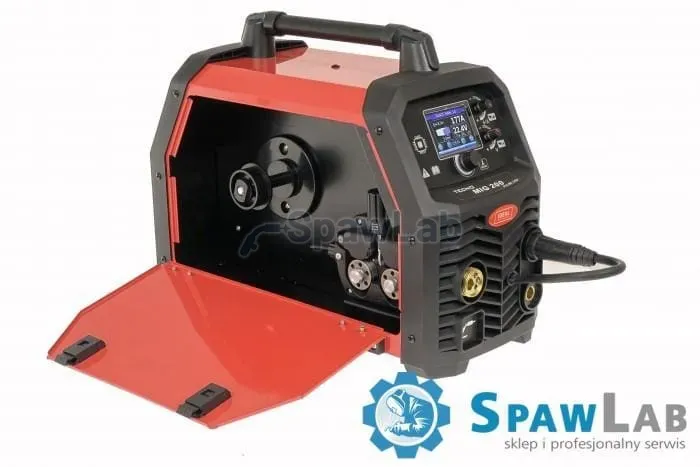
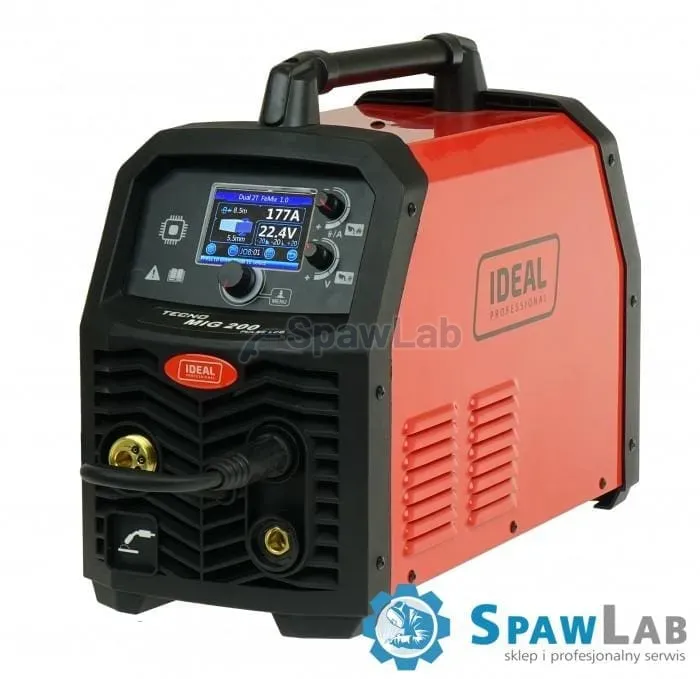
TECNOMIG 200P PULSE is a microprocessor-controlled synergic inverter MIG welder. It welds MIG/MAG, FLUX, MMA and TIG Lift, and brazes galvanised sheet. It suits aluminium and its alloys, stainless steel, and carbon and low-alloy steels. It runs on a 230 V supply, delivers up to 200 A and has a 4-roll wire feeder.
Specifications
- Power supply: single-phase 230 V, 50 Hz (1ph), with plug
- Mains protection: C25A
- Power: 6.5 kW
- Open-circuit voltage: 71 V / 13 V (VRD)
- Welding current range: 28 to 200 A (MIG), 16 to 200 A (MIG PULSE), 5 to 200 A (TIG/MMA)
- Maximum current: 200 A
- Current at 100% duty cycle: 160 A
- Current at 60% duty cycle: 200 A (MIG), 180 A (TIG/MMA)
- Wire diameter: steel 0.6 to 1.0 mm, stainless steel 0.6 to 1.0 mm, aluminium 0.8 to 1.2 mm, self-shielded 0.8 to 1.0 mm, brazing 0.8 mm
- Electrode diameter: 1.6 to 4.0 mm
- Wire feeder: 4-roll
- Wire spool: D100 (0.45 kg and 1 kg), D200 (2 kg and 5 kg)
- Parameter memory: 35 slots
- Protection rating: IP 23S
- Weight of machine / set: 12.5 / 16 kg
- Dimensions (L x W x H): 510 x 230 x 370 mm
- Packaging dimensions: 550 x 250 x 385 mm
- Warranty: 12 months for professional use, door-to-door service with no transport costs
Features
MIG/MAG synergic
You have three synergic MIG/MAG modes: MIG, MIG PULSE and MIG DOUBLE PULSE. You set parameters manually or choose one of 52 synergic programs for AlMg, AlSi, Al99.5, CuSi3, CuAl9, 308LSi, 316LSi and FE wires. The shielding gas (inert, active or a mixture) depends on the program chosen on the panel.
MIG pulse
Pulse controls the amount of heat put into the workpiece. The weld comes out better in every welding position, and there is less spatter.
Trigger modes and memory
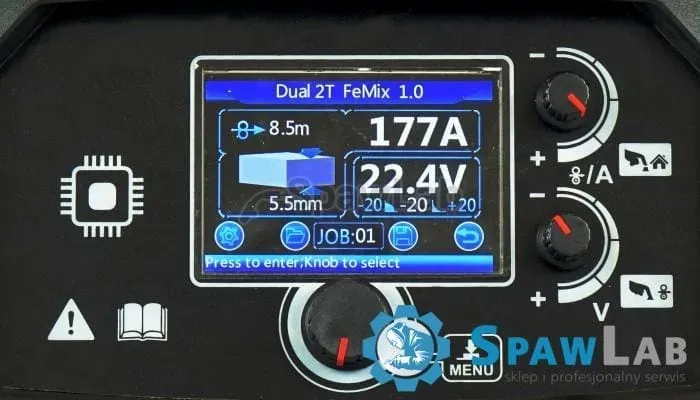
In MIG and MIG PULSE the torch trigger works in Spot (spot welding), 2-step, S2-step, 4-step (trigger latch for long welds) or S4-step mode. You save parameters in 35 slots. When you change gas and wire, you do not set everything up again.
Settings on the LCD display
In MIG you set inductance, current rise and fall (S2-step, S4-step), start and end current, wire burnback and run-in, pulse voltage (peak), pulse frequency and duty, and gas pre-flow and post-flow time. For spot welding you set the weld time (SPOT) and the pause between welds (CSPOT). In TIG LIFT you adjust pulse frequency, duty and current.
MMA functions
MMA PULSE controls temperature and current density, so the weld is better, with less spatter and dust. ARC FORCE (manual short-circuit current adjustment) helps electrode droplet transfer and stops the arc going out. HOT START (manual adjustment) gives a higher current at each ignition. ANTI STICK switches off the welding voltage when the electrode sticks to the material.
VRD, cooling and protection
VRD (Voltage Reduction Device) lowers the open-circuit voltage on the electrode to a safe level. This protects you against electric shock when you work in damp surroundings. A fan cools the machine, and overload protection guards it against damage.
Included
- MIG 24 welding torch, 3 m, fitted for aluminium
- Electrode cable, 2 m
- Earth cable, 2 m
- Wire feed rolls: 1.0 to 1.2 for aluminium and 0.8 to 1.0 for steel