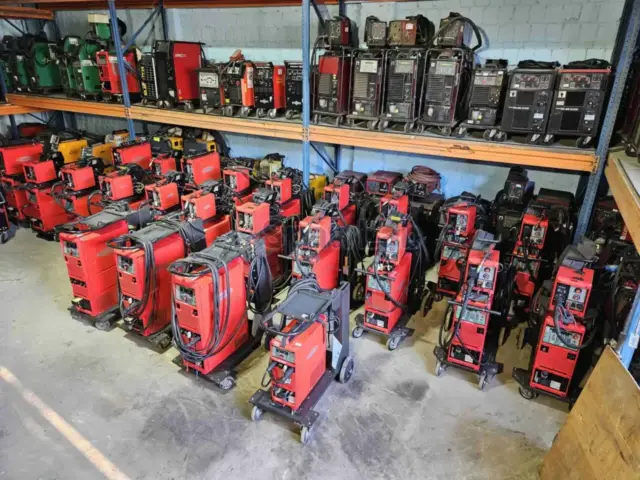
The Oerlikon Citotrans 501 is an inverter MIG/MAG power source with pulse, built on the TransArc system of Fronius design, liquid cooled and supplied from a 400 V mains. The maximum welding current is 500 A and you set it steplessly with a potentiometer. The machine handles wires of 0.8 mm, 1.0 mm, 1.2 mm and 1.6 mm diameter.
What this machine is for
This is a power source for three shift work. The synergic programs with a pulsed arc cover steel, CrNi stainless steel in the 99/1 mixture, AlMg5, AlSi5, Al 99.5 aluminium and the Al/Cu alloy. You pick the material and the wire diameter from the table under the panel cover, and the circuit sets the arc dynamics, so the typical defects fall away, that is lack of fusion and porosity on aluminium.
The documentation points to three areas of work: aluminium structures with the AlMg5 and AlSi5 programs, where the pulse narrows the heat affected zone, the chemical and food industry with stainless steels, and shipyards and heavy steel structures, where you use the MMA mode at the full 500 A and wire of 1.6 mm diameter. The Dynamik and Puls-Voltage potentiometers correct the hardness of the arc for a forced position or a wider gap.
Features and equipment
- Transistor inverter in the TransArc system: a Fronius design with stepless current control by a potentiometer up to 500 A.
- Synergic programs with a pulsed arc: steel, CrNi 99/1, AlMg5, AlSi5, Al 99.5 and Al/Cu, picked from the table under the panel cover.
- Dynamik and Puls-Voltage potentiometers: hand correction of the arc hardness and of the pulse voltage for forced positions and wider gaps.
- Work with wires of 0.8 mm, 1.0 mm, 1.2 mm and 1.6 mm.
- MMA mode at 500 A: covered electrode and gouging.
- Integrated liquid cooling circuit: work with water cooled torches at currents of about 400 to 500 A without overheating the torch and the current and water hoses.
Technical data
| Brand | Oerlikon |
|---|---|
| Model | Citotrans 501, TransArc system |
| Power source type | transistor inverter, MIG/MAG with pulse |
| Maximum welding current | 500 A, stepless control by a potentiometer |
| Synergic programs | steel, CrNi 99/1, AlMg5, AlSi5, Al 99.5, Al/Cu |
| Wire diameters handled | 0.8 mm, 1.0 mm, 1.2 mm, 1.6 mm |
| MMA method | up to 500 A, heavy welding and gouging |
| Supply voltage | 400 V |
| Cooling | liquid, integrated circuit |
What to watch out for
A 400 V supply needs a power socket and a circuit sized for the draw at 500 A. You check the cooling circuit before the first weld, because a broken flow damages the torch and the current and water hoses. To work you need a wire feeder, a liquid cooled torch and cables, and the source description does not name the contents of the set, so confirm it before you buy together with the program table under the panel cover.
The programs are tied to given materials and wire diameters, with another filler or another gas mixture you correct the parameters by hand with the potentiometers. No weight is given, arrange the transport before collection.
How we sell used machines
This unit was checked in our service workshop in Krotoszyn with measurements to PN-EN 60974-4 and a load test. The price includes the first year of the basic service package: an inspection with cleaning of the machine and a validation measurement. Further years can be added. We ship across the European Union, collection in person by appointment.