Presentation, video
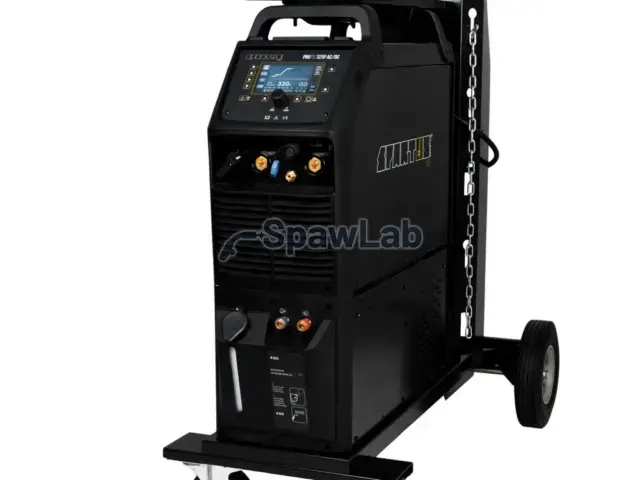
The POWER TIG 315 SYNERGIA AC/DC HF/LIFT PULS AQUA inverter welder is built on IGBT technology with PWM and MCU components, for welding by
TIG AC/TIG AC PULS/ TIG DC/TIG DC PULS/ TIG MIX (AC+DC) on direct current (DC) or alternating current (AC), and by MMA with covered electrodes on direct current (DC) or alternating
(AC). It is intended for welding all metals, aluminium and brass included.
The welder runs in 2-stroke and 4-stroke mode with non-contact (TIG HF) or contact arc striking (LIFT). It stores 6 individual sets of
welding parameters in memory and it accepts external control of the welding process.
An intuitive graphic menu on the colour LCD display makes setting the working parameters quick and easy:
, welding current with a gas cooled torch (10-250 A)/liquid cooled torch (10-315 A)
, gas pre-flow time before the arc is struck (0.1-10 s)
, start current (5-315 A)
, welding current up slope time (0-10 s.)
, base current, only in TIG DC PULS mode (10-315 A)
, pulse width (duration), only in TIG PULS mode (5-100%)
, pulse frequency, only in TIG DC PULS mode (0.5-200 Hz)
, AC balance (10-50%)
, AC frequency (25-250 Hz, values vary with the welding current)
, current down slope time (0-10 s.)
, end current (5-315 A)
, gas post-flow time after the arc goes out (0.1-10 s.)
, HOT START (40-315 A)
, MMA parameters: ARC FORCE (0-10), ARC LENGTH (0-10), ARC START (0-10)
The welder has a synergic function (TIG AUTO SET) that covers:
, material selection (Fe/Al/SS)
, electrode diameter selection
, thickness of the material being welded
A choice of AC waveform (square, sine and triangular wave) lets you
work on the weld and its appearance precisely.
The TIG PULS function prevents burn-through when welding thin material
(below 1.5 mm thick) and discolouration of the material (when welding stainless steel).
Two carrying handles make it convenient to change the place of
work. The broad set of functions and simple operation suit workshop and industrial jobs
with a large share of non-ferrous metal welding.
Equipment
Standard equipment:
, power lead 3 m without a plug
, PROFI TIG WP 18 welding torch 4 m (DX50) with plugs for the liquid connection (red, blue)
, earth lead 4 m with a 300A clamp (DX50)
, PU gas connection hose 3 m
, gas connector (nipple) for a type 21 quick coupling
, 5-pin torch control socket
, torch gas connection, type 21 quick coupling
, coolant sockets, type 21 quick couplings (red, blue)
, liquid cooling unit
, transport trolley with a shelf and front swivel wheels with a brake
Technical data
| Code | 104 417 |
| Machine type | POWER TIG 315 AC/DC |
| Supply voltage [V] | 400 |
| Open circuit voltage [V] | 50 |
| Welding current range [A] | TIG AC 10-315 TIG DC 5-315 MMA 5-270 |
| Max duty cycle EN 60974-1 | 315A@60% 220A@100% |
| Power source dimensions[cm]Source with trolley[cm] | 62x25x45 96x49x108 |
| Power source weight [kg] | 26 |