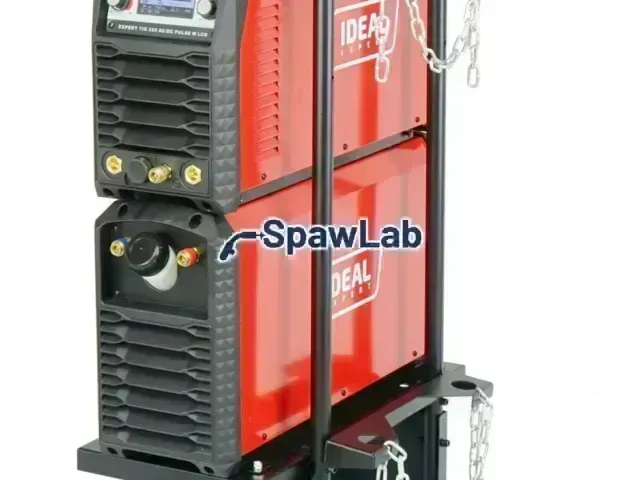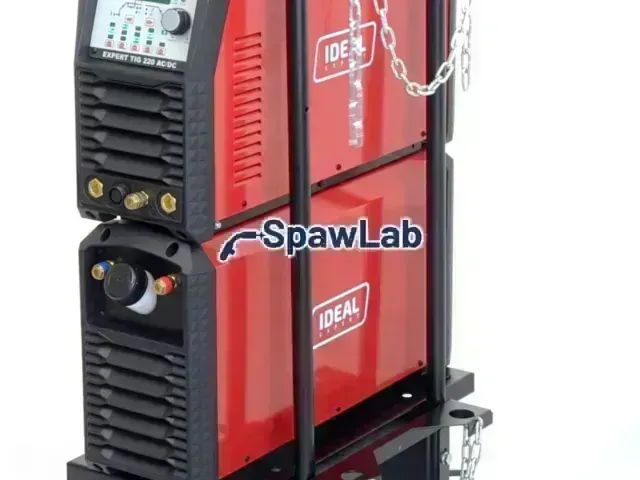

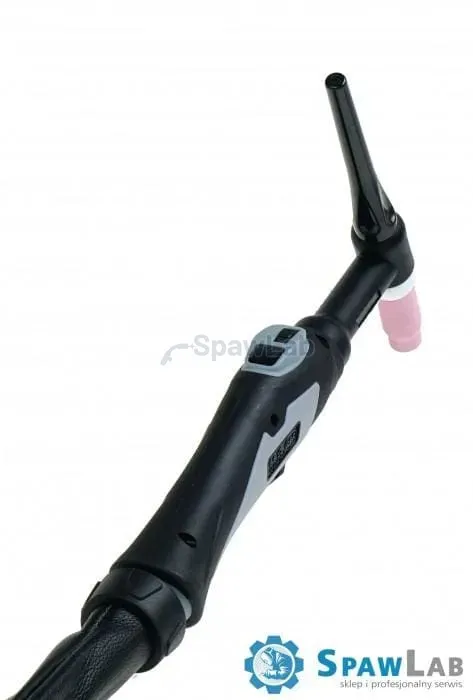
Expert TIG 422 AC/DC Pulse Pro7 LCD is an IGBT inverter welder for TIG AC/DC (including pulse), TIG spot and MMA AC/DC, with MULTITACK, DYNAMIC ARC, TIG MIX and RPT modes. TIG welding current reaches 420 A, so you can weld stainless and carbon steel, aluminium alloys, brass and titanium. The LCD touchscreen and SMART TIG mode make operation simpler, also when you have less experience. It suits production and service workshops, repair work and demanding hobby projects.
Specifications
- Welding processes: TIG AC, TIG DC, TIG MIX, TIG spot, MULTITACK, MMA AC, MMA DC, MMA PULSE, pulse modes and RPT
- Power supply: three-phase 3×400 V, 50/60 Hz
- Control panel: Pro7 LCD touchscreen with extended settings (SMART TIG, MultiWAVE, Cap Shaping)
- Arc ignition: contactless HF or contact LIFT, your choice
- Cooling: liquid cooling available (built-in cooler), recommended for long work at high current
- Torch trigger modes: 2T, 4T, RPT (two current levels), spot (SPOT)
- MMA functions: HOT START, ARC FORCE, ANTI STICK
- Protection: short-circuit, thermal
- Warranty: 12 months for professional use, door-to-door service
Features
TIG DC and TIG DC PULSE: stainless steel, carbon steel, copper alloys
TIG DC welds with direct current. It is the basic mode for carbon and stainless steels and other materials that need stable penetration and a uniform weld structure: the weld pool is easy to control and there is less spatter. In TIG DC PULSE the current alternately rises and falls, so less heat goes into the material. On thin sheet and parts prone to distortion, pulse reduces the risk of burn-through.
TIG AC and TIG AC PULSE: aluminium and brass
Alternating current cleans oxides from the aluminium surface, the arc is stable and penetration is strong. You adjust AC balance and AC frequency, that is, the depth of penetration and the degree of cleaning. Pulse in AC doses heat through periodic current drops, so thin aluminium and brass sections distort less and discolour less often.
TIG spot (SPOT)
The function makes very short, precise tack welds before the actual welding, for example when tacking structures in automotive work and production. A short tack on the sheets limits distortion. Tacking is simple and fast, and you do not have to hold parts in one position for long. On aluminium and thin-walled steel, SPOT limits overheating of the material.
MULTITACK: intermittent welding
This mode, also called cold welding, interrupts the arc cyclically, and you join the material with short, regular pulses. It is used, among other things, in precision work and in aviation. Breaks in heat input reduce stress and the risk of distortion, and with uneven arc guidance it is easier to avoid overheating. You adjust the cycle frequency (e.g. 0.5 to 6.0 Hz).
TIG MIX: aluminium with cleaning and deep penetration
The welder combines direct (DC) and alternating (AC) current into one hybrid waveform. You get full penetration and effective cleaning in one process, without changing modes during work. One setup covers more tasks, so it is easier to avoid wrong parameters. Aluminium assemblies go faster, and welds are more uniform and neat, which matters in decorative and industrial projects.
TIG RPT and DYNAMIC ARC
RPT (Repeat) switches in real time between two programmed current levels, e.g. main current and base current. It helps on long runs of varying thickness, in difficult positions and at edges that overheat easily. DYNAMIC ARC fine-tunes the arc to keep the correct weld width, so there is less grinding and rework. If you briefly move the electrode away, the welder corrects the parameters itself and the arc does not go out.
MMA AC/DC and MMA PULSE
With a coated electrode you weld on direct (DC) or alternating (AC) current, e.g. with electrodes for aluminium and special alloys. This is handy for small repairs of aluminium structures on site, where TIG preparation takes too long. MMA PULSE supports droplet transfer: there is less spatter, the weld pool is easier to control in difficult positions, and the arc does not go out so easily with small errors in electrode guidance.
LCD touchscreen
The screen shows all parameters, from start current through AC balance to HOT START and ARC FORCE in MMA mode. You have dozens of settings at hand, including MultiWAVE, Cap Shaping and successive pulse phases. You save settings in the machine memory, so setup takes less time on repeat jobs. Despite the many options, you will learn to use it quickly.
SMART TIG: synergic mode
You enter the material, thickness, gas type and process (AC/DC), and the welder suggests parameters. Then you can adjust them to suit you. The machine tells you how to avoid overheating and weld cracking. There are fewer failed attempts and less wasted material, and learning takes less time.
Cooler and housing
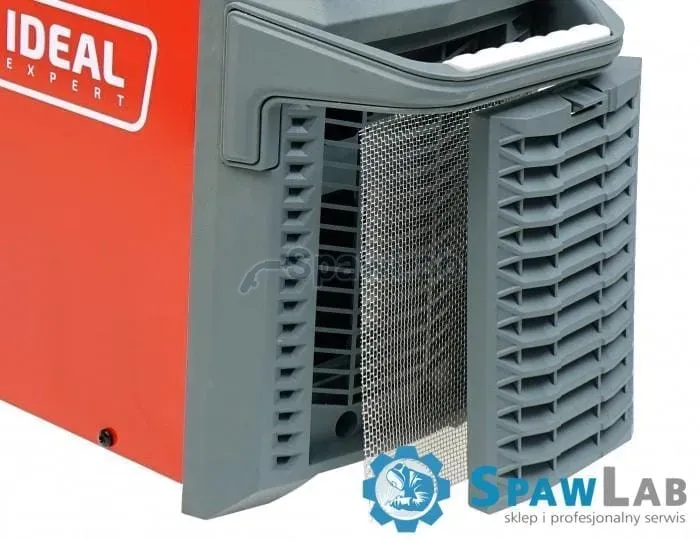
The machine usually comes with a liquid cooler. With it you weld longer at high current without overheating the torch and power source, and without breaks due to thermal overload. The housing is compact for a power source of this output and designed with ergonomics in mind, and short-circuit and thermal protection extend the service life of the set.