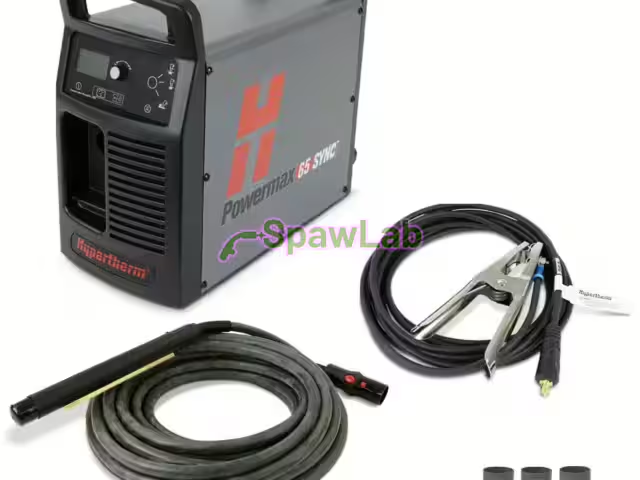
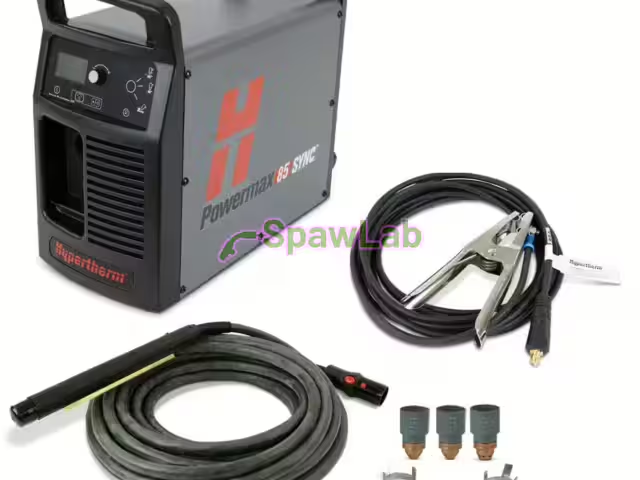
Hypertherm Powermax 65 is an inverter plasma cutter running on compressed air, supplied from a three phase 400 V mains. You set the cutting current from 20 to 65 A, and the manufacturer gives quality cutting of steel up to 20 mm, maximum cutting 25 mm and severing from the edge up to 32 mm. The whole unit with a torch on a 7.6 m lead weighs 26 kg, so you carry it without a trolley.
What this machine is for
Plasma cuts every metal that conducts current, so beyond black steel you handle stainless steel and aluminium with this machine, where an oxygen torch is of no use. Powermax 65 parts sheet to a quality standard up to 20 mm, that is with a straight edge that needs no grinding of the excess. The maximum thickness is 25 mm, and severing from the edge reaches 32 mm and serves to part the material when the kerf may be uneven. The manufacturer allows piercing in the middle of the sheet up to 16 mm, above that thickness you start the cut from the edge so as not to melt the nozzle. These four numbers, 20, 25, 32 and 16 mm, describe completely different tasks and it is worth telling them apart when you plan production, because an edge after maximum severing almost always goes to the grinder afterwards.
The second function is plasma gouging. After you change the front shield parts for directional nozzles the jet hits the material at an angle and blows the liquid metal outwards. That is how you remove corrosion, cut down excess and dig out weld defects before the joint is welded again. Gouging uses more air than cutting, the documentation gives 212 litres per minute for this mode.
The machine suits halls that part sheet in series, assembly and service teams that carry equipment to a site, and workshops that take apart multi layer structures and lattice frames. The pilot arc hold circuit does not go out when the torch runs off the material, so you cut reinforcing mesh, fences and frames without striking again at every bay. At a CNC table the same unit works once a machine torch is plugged in. Plasma cuts faster than an oxygen torch on thin and medium sheet, leaves a narrow heat affected zone and distorts the part less, and a kerf made with a correctly chosen nozzle is fit for welding at once.
Features and equipment
- Inverter build on IGBT transistors: at a current up to 65 A the whole unit with the torch weighs 26 kg.
- Cutting current control from 20 to 65 A: lower settings for thin sheet and less nozzle wear, higher ones for thick plate.
- FastConnect coupling: you change the hand torch for a machine one without tools, so the same power source serves a manual station and a CNC table.
- Torch from the Duramax family: a reinforced housing of high impact polymers and coatings that insulate the handle from the heat when cutting 32 mm plate, and the head centres the wear parts itself.
- SpringStart ignition: the arc starts mechanically, by a spring system, without a high frequency module, so the machine does not disturb CNC controllers or electronics next to it.
- Smart Sense gas automation: the system picks the pressure itself for the length of the connected lead and for the set current, which protects the electrodes against burning out the core.
- Pilot arc hold: when cutting open work material the arc comes back after the torch runs into a gap, without striking again.
- Plasma gouging mode: after you change the nozzles for directional ones you blow the liquid metal out of the groove with a stream of 212 litres of air per minute.
- Cutting of every metal that conducts current: beyond black steel you work stainless steel and aluminium, also painted and corroded parts, which an oxygen torch does not cut.
- Three phase 400 V supply: the draw is spread over three phases, so at the full cutting current the voltage in the installation stays steady.
Technical data
| Brand | Hypertherm |
|---|---|
| Type | inverter plasma cutter |
| Supply | 400 V, 3 phases, 50 to 60 Hz |
| Cutting current | from 20 to 65 A |
| Quality cutting thickness | 20 mm |
| Maximum cutting thickness | 25 mm |
| Maximum severing from the edge | 32 mm |
| Piercing capacity | 16 mm |
| Duty cycle 50% at 40 degrees C | 65 A |
| Duty cycle 100% at 40 degrees C | 46 A |
| Air flow and pressure when cutting | 189 l/min at 5.9 bar |
| Weight with a torch on a 7.6 m lead | 26 kg |
| Cooling | gas |
What to watch out for
For work you need two things: a three phase 400 V mains at a frequency of 50 or 60 Hz and an efficient compressor. Cutting draws 189 l/min at 5.9 bar, gouging 212 l/min, and the air has to be dry and free of oil. Moisture and oil in the installation shorten the life of nozzles and electrodes faster than the current itself, so it is worth having a dryer and a filter ahead of the machine. The duty cycle at 40 degrees C is 65 A at 50% and 46 A at 100%, so at the full current half of the time goes to cutting and half to cooling.
Nozzles, electrodes and shields are consumables that wear in normal work, so before the first cut check their state and count a stock for the start. The same torch moves between cutting and gouging after a change of parts. A weight of 26 kg together with the torch means one person carries the machine, and the torch lead 7.6 m long gives reach around the station without moving the power source. You match the travel speed of the torch to the thickness: a torch led too slowly leaves dross on the lower edge, too fast it does not cut the material right through. You hold the distance between the nozzle and the sheet with a spacer guide, because the angle of the edge depends on it.
How we sell used machines
This unit was checked in our service workshop in Krotoszyn with measurements to PN-EN 60974-4 and a load test. The price includes the first year of the basic service package: an inspection with cleaning of the machine and a validation measurement. Further years can be added. We ship across the European Union, collection in person by appointment.