


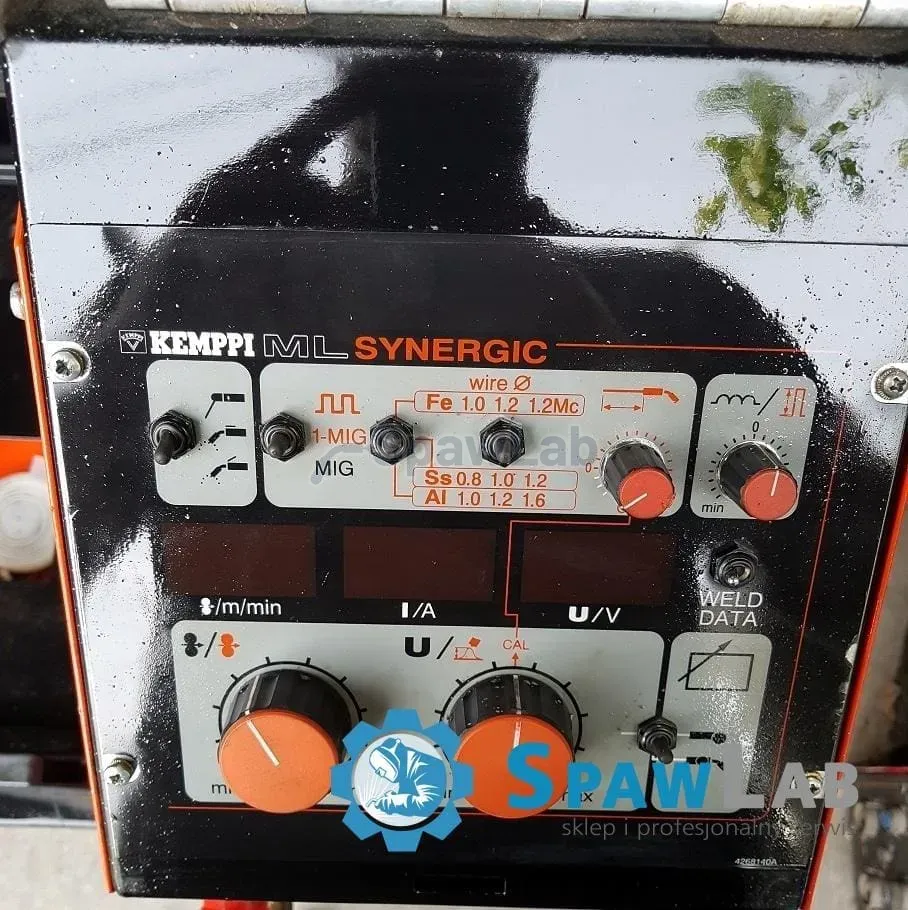


The Kemppi Pro 4000 Puls is an industrial MIG/MAG power source with pulse and a welding current up to 400 A, supplied from a 400 V mains. The set has a Procool 10 liquid cooler, an external Promig 500 feeder and an MLS panel. The weight of the set is 120 kg.
What this machine is for
A current of 400 A handles thick steel sheet and multi shift work without overheating the power source. Resistance to swings of voltage in the hall mains means that the parameters hold also when another machine starts next to it. This is a set for makers of heavy steel and bridge structures, shipyards, making of pressure tanks and pipelines and service shops for construction machines and farm equipment.
Pulse orders the transfer of metal in the arc. There is less spatter, so less cleaning is left after welding, and lower heat input protects thin materials against distortion, with deep penetration kept in thick elements. Where the look of the joint counts at full strength, this is the basic working mode.
On aluminium the synergic programs together with pulse give a weld with a look close to the TIG method at the output of a wire welder. Arc stabilisation in the pulsed mode limits porosity and lack of fusion at the start of the run, that is the two typical problems in welding aluminium with a classic arc. From there such a set went to boat building workshops, makers of tanks and firms building bodies of special vehicles, next to workshops working on stainless steel.
The MLS panel, that is Multi Logic System, has ready programs for black steel, stainless steel and aluminium, so a change of material is a choice of a program, and not putting the parameters together from zero. Digital readings show the current and the voltage in real time, so you have control over the process and repeatability in line with the demands of quality control in the plant.
The build is modular. The power source, the cooler and the feeder are separate modules, so you move the feeder away from the power source and widen the working reach on large sizes and on space structures. Service and extension go by modules, and for transport you split the set into parts instead of carrying the whole in one piece.
Liquid cooling is a condition here, and not an addition. The thermal stability of the whole circuit translates straight into the penetration and into the look of the face through the whole working day, so in automated processes and on aluminium alloys the cooler works together with the power source from the first to the last weld. Active removal of the heat also protects the wear parts of the torch, which in welding at a high current go down the fastest.
The feeder stands on a trolley, so together with the torch you move it around the part and you do not drag the cable package in an arc across half the hall. Fewer bends of the torch means an evener wire feed and fewer breaks in the arc, and with aluminium wire the difference shows at once. The ergonomics of the station come down here to a level where the welder does not lose time on moving the cables.
Typical uses are the production of heavy steel and bridge structures, the shipyard industry together with the building of aluminium hulls, the making of pressure tanks and pipelines, service shops for construction machines, repairs of farm equipment and craft workshops working on stainless steel. The common point is a current of 400 A, pulse and the demand for repeatable quality of the weld.
Features and equipment
- MIG/MAG welding with pulse. A controlled transfer of metal limits spatter and the heat input, and the penetration in thick elements stays deep.
- Synergic programs for aluminium. Together with pulse they give a clean weld without porosity and without lack of fusion at the start of the run, that is without the two most common faults in welding light alloys.
- MLS control panel (Multi Logic System). Ready programs for black steel, stainless steel and aluminium and digital readings of the current and the voltage in real time.
- Arc stabilisation. The circuit corrects the parameters when the length of the wire stick out changes, so the fusion and the face stay even also in forced positions.
- Adjustment of the arc dynamics. You move the characteristic from soft, with a smaller depth of penetration, to hard and strongly penetrating for thick structural welds.
- External Promig 500 wire feeder. A solid drive gives an even feed whatever the length of the torch and leads steel wires and soft aluminium wires without deforming them in the guides.
- Procool 10 liquid cooler. It holds the temperature of the torch in welding with high currents in a continuous cycle, protects the wear parts of the torch and steadies the parameters of the arc.
- Modular build. You place the power source, the cooler and the feeder around the station, service and move them separately, and you extend the set without a change of the power source.
- Resistance to swings of voltage in the mains. The parameters of the arc hold also when the load of the switchboard changes during the shift, which in multi shift work happens all the time.
Technical data
| Brand | Kemppi |
|---|---|
| Process | MIG/MAG with pulse |
| Maximum welding current | 400 A |
| Supply | 400 V, three phases |
| Type of cooling | liquid, Procool 10 |
| Feeder model | Promig 500 |
| Control panel | MLS with pulse |
| Weight of the set | 120 kg |
What you get
- Kemppi Pro 4000 power source
- Procool 10 liquid cooler
- external Promig 500 wire feeder
- MLS control panel with pulse
What to watch out for
The supply is 400 V, three phases, a power connection is needed with a fuse matched to the draw at the upper settings. Liquid cooling calls for handling: you watch the fluid level, the flow and the tightness of the quick couplings of the torch, and after a longer break in work you also check the state of the fluid in the tank. The weight of the set is 120 kg, so plan the transport on a pallet and the unloading with a forklift.
The card does not list a welding torch or an earth cable, you pick this equipment separately for the current and the length of the bundle. The card does not give the length of the interconnection cable or the duty cycle at the single currents, confirm this data before you buy if you plan continuous work at the maximum. For aluminium you add rolls for soft wire and a liner in the feeder.
This unit is sold
This machine has already gone to a customer. Similar units are listed below, and if you want the same model, leave your contact details in the form and we will let you know when the next one arrives.