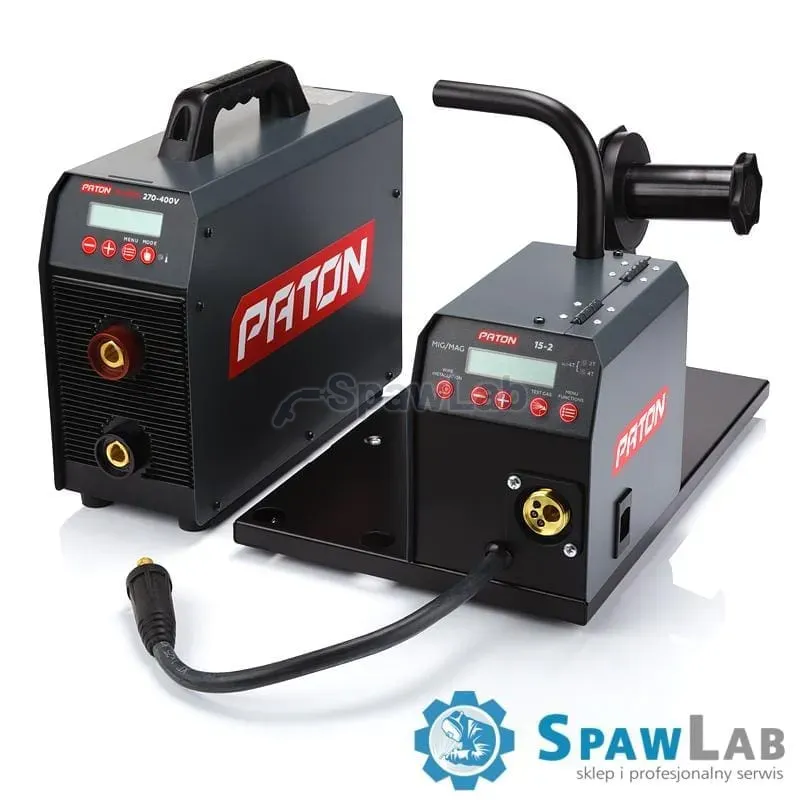
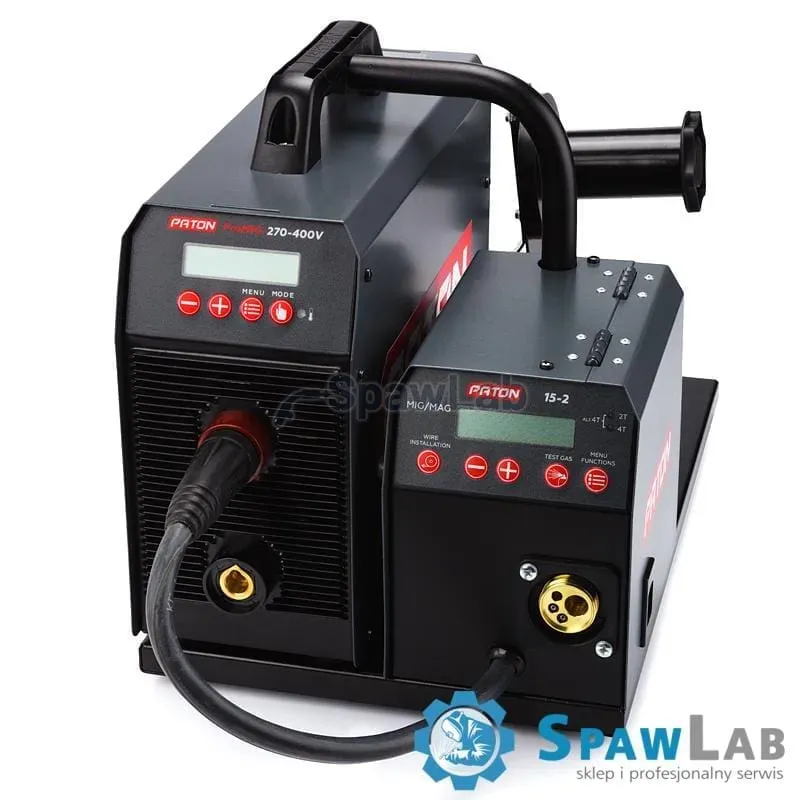
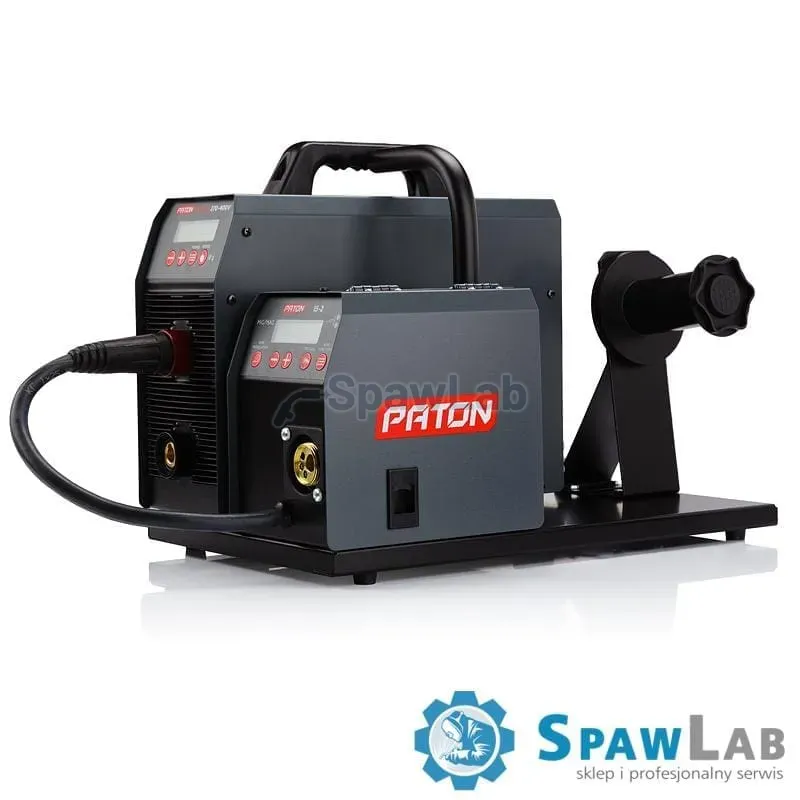
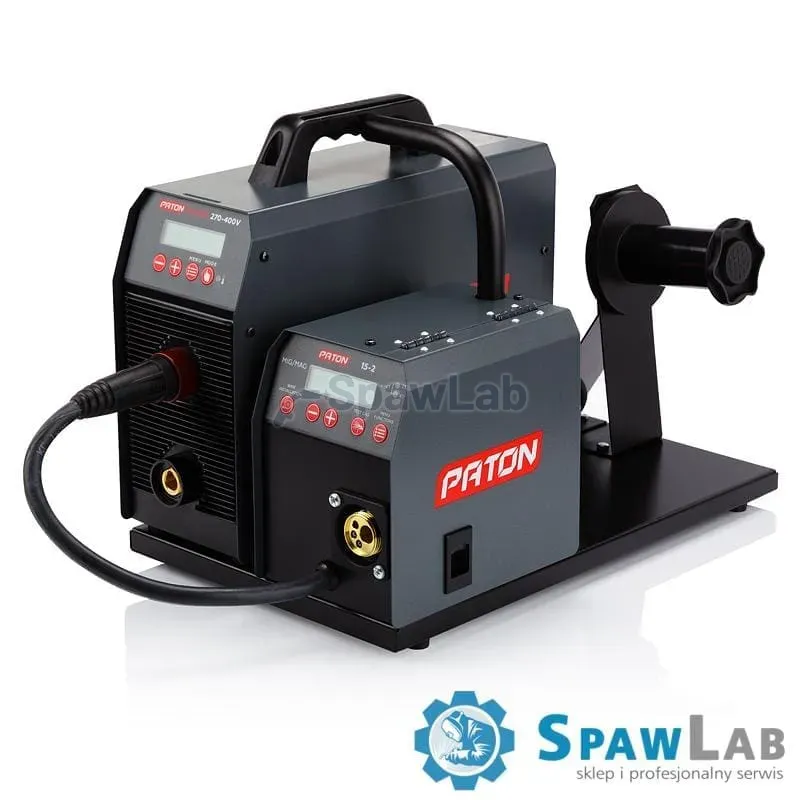
Paton ProMIG 270 15-2 400V MIG/MAG welder, key facts
The Paton ProMIG 270 15-2 400V MIG/MAG welder is built for semi-automatic MIG/MAG welding under shielding gases and gas mixtures, for manual MMA arc welding and for DC TIG arc welding under argon.
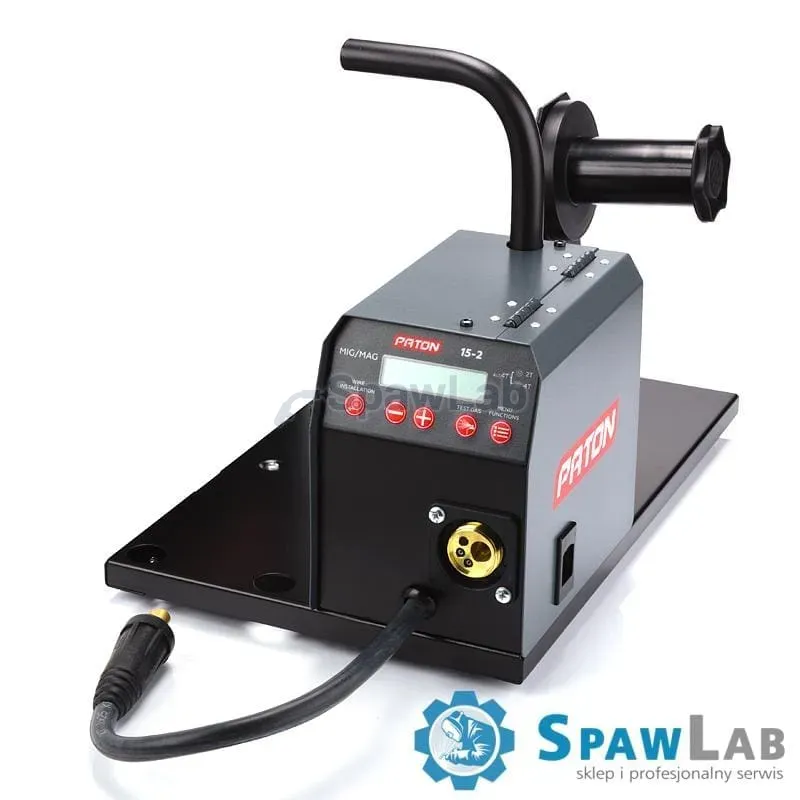
The design of the ProMIG 270 15-2 (15 kg spool, which also takes a 5 kg spool, 2 roller feeder) gives one of the best levels of protection against outside conditions on the market. The rated current of this model, 270A at a 70% duty cycle, allows intensive welding of 6 mm material without the risk of overheating. The power source can be separated from the wire feed unit, both for comfort of use and for safety. A hallmark of the semi-automatic machines in the PATON™ series Professional is the high quality sealed metal wire feeder, together with the KZ-2 connector of the EURO type, a worldwide standard that lets you fit a different torch later as you see fit.
In a fully electronic system the control unit has all the resources of the power source at its disposal, within its full output and no matter which method is in use. The Professional series machine is meant for industrial use and for the most demanding users.
Functions and features of the Paton ProMIG 15-2 270 400V MIG/MAG welder
GASLESS WELDING, WELDING WITH SELF SHIELDED WIRE
All PATON MIG/MAG welders are prepared for welding with self shielded wire. Unlike the standard MIG/MAG process, this kind of welding runs without shielding gas, but it does call for a special welding wire. Such wire produces its own shield, which helps to protect the welding arc.
BRAZE WELDING, INDUCTANCE CONTROL
Paton MIG/MAG welders of the Standard and PRO series can braze weld thanks to inductance adjustment in three steps. Inductance control lets you match the arc characteristic to the thickness of the workpiece. This function is needed to change the rate of current flow when the arc voltage changes. The thinner the part to be welded with MIG/MAG, the higher the inductance should be (soft arc, shallower penetration), and for thick parts the opposite applies (hard arc, deeper penetration).
PULSE FUNCTION IN EVERY METHOD
PULSE in the TIG method, full control of the heat put into the material, a very good function for welding stainless and acid resistant steel,
PULSE in the MMA method, easier transfer of material from the electrode into the weld pool, better quality of the welded joint,
PULSE in the MIG/MAG method, easier detachment of the metal droplet from the tip of the electrode wire, with adjustable pulsed current parameters. Pulsed MIG welding is useful on stainless and acid resistant steels and on aluminium alloys. Pulse welding also gives better results when braze welding CuSi3
MAIN DIFFERENCES BETWEEN THE STANDARD AND PRO SERIES MIG/MAG WELDERS:
- duty cycle, PRO series welders have a 70% duty cycle, while the Standard series has a 45% duty cycle at the same welding current. PRO series welders also reach continuous duty at a higher welding current than Standard series welders.
- wire feeder, the PRO series has a separate wire feeder that takes spools from 15 to 18 kg. The feeder can be detached from the power source for comfortable welding with other methods, for example MMA or TIG DC. The PRO series also comes in 2 roller and 4 roller feeder versions. In Standard series welders the feeder is built into the machine, takes only a spool up to 5 kg and always has two rollers.
Main advantages of the Paton ProMIG 270 15-2 400V MIG/MAG welder
- European production
- Electronic thermal protection system guarding every heat generating component against overheating
- Dependable operation thanks to IGBT technology
- Works on long extension leads and with a generator
- Welding with pulsed current in every welding method
- Improved stability of the electric arc
-
Switching between 2T and 4T modes, gas purge from the feeder function
- The machines have protection against voltage surges and a stabilising circuit, which keeps them working correctly across the voltage range
- Half the electricity demand compared with conventional power sources
- Correct fusion and bead shape regardless of welding position
3 year manufacturer warranty for consumers and for companies
Build quality confirmed by a 3 year DOOR-to-DOOR manufacturer warranty. Models in the PRO series have a compact design with a number of technical solutions that make the machines less prone to failure. Inverter reliability in dusty and humid surroundings has been increased.
The set you buy contains:
- MIG/MAG welder PATON™ ProMIG 270 (15-2) 400V
- Wire feeder PATON™ BPI 15-2 (15 kg spool, which also takes a 5 kg spool, 2 roller feeder)
- Electrode holder ABICOR BINZEL DE2200 3m
- Earth clamp ABICOR BINZEL MK300 3m
- Wire feed rollers 1x (0.6-0.8), 1x (1.0-1.2) V
- Gas quick coupling
- Cardboard packaging
- Carrying strap
- User manual
Main advantages:
- Broad adjustment of welding parameters:
, MMA method, 1 (basic) + 10 (additional)
, TIG method, 1 (basic) + 10 (additional)
, MIG/MAG method, 2 (basic) + 8 (additional) - Welding with pulsed current, which is also programmable, in every welding mode;
- Besides protection against mains surges, the machines have a stabilising circuit for longer voltage swings in the single phase mains and keep working correctly across the voltage range from 320 V to 440 V.
- Matched to the standard mains supply. Thanks to its high efficiency the power source
needs half the electricity compared with conventional sources; - Automatic fan speed control: the fan runs harder when the machine is hot and slows down when the machine is idle. This cuts fan wear, the amount of dust inside the machine and the noise during welding
- Comfortable work with the machine loaded at its rated current, with no
need for cooling breaks at 25 °C. - High reliability in production conditions with heavy dust and high
humidity. - Longer life thanks to impregnation of the electronics with two layers of high quality varnish, which keeps the product dependable throughout its service life.
- The welder has an electronic thermal protection system guarding every heat generating part of the welding unit against overheating.
- Improved stability of the electric arc.
- Stepless adjustment of welding parameters.
Efficiency thanks to the latest advanced IGBT technology.
| Supply voltage 50/60 Hz | 3×400 V |
| Required mains fuse | 11A |
| Rated welding current | 270 A |
| Maximum welding current | 350 A |
| Duty cycle, % | 70%, 270 A 100%, 220 A |
| Supply voltage variation range | ±15% V |
| Welding current adjustment range | 14-270 A |
| Welding voltage adjustment range | 12-29 V |
| Wire feed speed adjustment range | 2.0-16 m/min |
| Covered electrode diameter | 1.6-6.0 mm |
| Number of pressure rollers | 2 |
| Solid wire diameter | 0.6-1.2 mm |
| Spool weight, no more than | ≤18 kg |
| Pulsed current welding methods | MMA/TIG/MIG/MAG |
| Hot-Start function in the MMA method | Adjustable |
| Arc-Force function in the MMA method | Adjustable |
| Anti-Stick function in the MMA method | Automatic |
| Open circuit voltage reduction circuit | On / Off |
| Open circuit voltage | 12 / 75 V |
| Arc striking voltage | 110 V |
| Rated power draw | 7.9-8.6 kVA |
| Maximum power draw | 11.0 kVA |
| Energy efficiency | 90% |
| Cooling | Automatic |
| Operating temperature range | 25 to +45 °C |
| Standards met: | EN 60204-1:2006 EN 60974-1:2012 EN 60974-10:2014 |
| Dimensions (length, width, height), mm: | 540 x 360 x 400 |
| Weight, kg | 23.5 |
| Protection rating | IP 33 |