


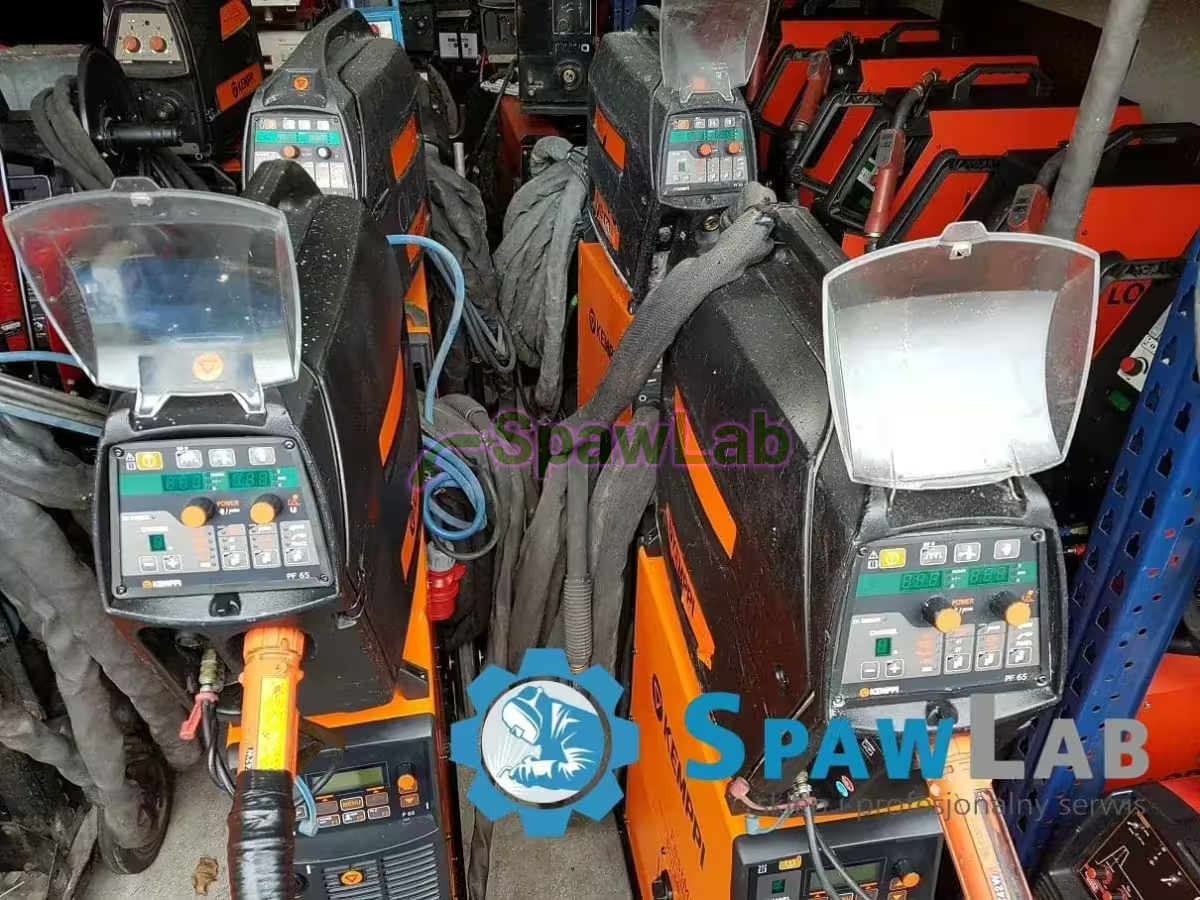




The Kemppi FastMig Pulse 450A in the Full Soft version is an industrial MIG/MAG power source with a current of 450 A at a 60% duty cycle and 350 A at a 100% duty cycle. The supply is 400 V, three phases, with an MXF 67 feeder, a FastCool 10 cooler and a PF 65 panel. In the package you have pulse, double pulse, WiseFusion and WisePenetration.
What this machine is for
This is a power source for MIG/MAG welding in production, where the quality of the weld and continuity of work count. A current of 350 A at a 100% duty cycle means welding through the whole shift without breaks for cooling, and 450 A at a 60% duty cycle gives a margin for thick elements. Power control holds the parameters also at swings of voltage in the hall mains, which matters in multi shift work.
Pulse and double pulse shape the face of the weld and control the amount of heat in the material. The result is a rippled face known from the TIG method at the output of a wire welder, so such a set was taken by plants welding aluminium, stainless steel and thin high alloy sheet, next to makers of steel structures and shipyards.
The build is modular. You separate the power source, the wire feeder and the cooling system, so transport, service and extension of the set are simpler, and a change of a single module does not call for touching the whole electronic circuit of the machine. The channel memory holds the settings, so you start repeatable joints with one choice.
On thick aluminium structures a current of 450 A together with pulse and the WiseFusion process gives penetration over the whole section without heating the material many times. On stainless steel the same package limits discolouring and distortion, because the heat input is lower than in welding with a classic spray arc. To that comes series production, in which the repeatability of the settings from the channel memory decides the acceptance of the part.
The housing and the power control circuits are made for work in a hall, multi shift as well. Swings of voltage in the plant mains do not translate straight into the arc, so the parameters stay in the technological window whatever the load of the switchboard. The set was taken by plants that had to weld without stops through the whole shift.
Features and equipment
- Pulse and double pulse. Double modulation of the current gives control over the pool and over the amount of heat, so thin aluminium sheet and high alloy steel do not distort, and the face comes out rippled.
- WiseFusion. The Kemppi process focuses the arc and holds it steady, so the penetration is deeper with less heat, and work in a narrow gap and in forced positions is easier. There is less distortion and less spatter.
- WisePenetration. It holds a constant penetration in spite of changes of the wire stick out, so in tight places the fusion is even along the whole joint and there are fewer corrections.
- MXF 67 wire feeder. Four guide rolls give an even feed, an aluminium housing protects the mechanism, and stepless adjustment of the pressure and exchangeable rolls handle steel wires and soft aluminium wires without deforming them.
- FastCool 10 cooler. An efficient pump and an ordered flow of coolant take the heat from the torch, so you weld with high currents for a long time, and the wear parts of the torch last longer. The circuit is synchronised with the work of the power source, so the pump does not run without need and the noise at the station is lower.
- PF 65 panel. A menu in Polish, a clear display with a reading of the current, the voltage and the wire feed speed and access to the saved programs and special functions. The handling is simple enough for bringing a new operator onto the station to take one shift.
- Channel memory. You call repeatable settings from the memory, which shortens the changeover in series production.
- Modular build. You separate the power source, the feeder and the cooler, so transport and service go by modules, and you extend the set later without a change of the power source.
- Work under a high load. A 60% duty cycle at 450 A handles long welding of thick elements without overheating the system.
Technical data
| Brand | Kemppi |
|---|---|
| Process | MIG/MAG with pulse |
| Maximum welding current | 450 A |
| Current at a 60% duty cycle | 450 A |
| Current at a 100% duty cycle | 350 A |
| Supply | 400 V, three phases |
| Mains fuse | 35 A |
| Wire feeder | MXF 67, four rolls |
| Cooling | FastCool 10, liquid |
| Control panel | PF 65, menu in Polish |
| Special processes | pulse, double pulse, WiseFusion, WisePenetration |
What you get
- Kemppi FastMig Pulse 450A Full Soft power source
- MXF 67 wire feeder, four rolls
- FastCool 10 liquid cooler
- PF 65 control panel
What to watch out for
The supply is 400 V, three phases. The card gives a mains fuse of 35 A, so you check the connection and the fuse links before you connect, and with a longer supply cable you look at the cross section of the cores. Liquid cooling calls for handling: you check the coolant level, the flow and the tightness of the quick couplings of the torch before every shift.
The card does not list a welding torch or an earth cable, you pick this equipment separately for the current and the length of the bundle. The set has many parts and is heavy, plan the transport on a pallet and the unloading with a forklift. The card does not give the weight or the dimensions of the modules, confirm them before collection.
This unit is sold
This machine has already gone to a customer. Similar units are listed below, and if you want the same model, leave your contact details in the form and we will let you know when the next one arrives.