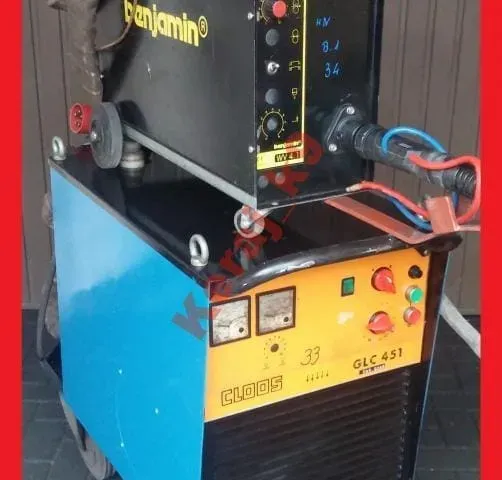
Cloos GLC 333 MC4 is an industrial MIG/MAG welder on an inverter source with MC4 digital control, with the source and the wire feeder in one housing. The working range runs from 5 A at 14 V to 330 A at 31 V, at a 40% duty cycle the machine gives 330 A, and at a continuous 100% load it gives 260 A at 27 V. Supply is 3 x 400 V at 50 Hz with a T16 A fuse.
What this machine is for
The machine joins classic MIG/MAG with a pulse process and a double pulse, so it handles aluminium, CrNi stainless steel, carbon and alloy steel and galvanised sheet. For aluminium and quality steels you reach for AluPlus, that is the double pulse with a wide set of settings: modulation frequency, duty indicator, pulse height and pulse width. That modulation lays a bead with a ripple close to a TIG bead and keeps the heat put into the material in check, so thin sheet neither burns through nor ripples.
On stainless steels, work in the pulse cycle limits heat tinting around the weld and shortens the finishing work, because less is left to brush and pickle. On carbon and alloy steel you work in the standard way or with synergy and get deep penetration with little spatter. Galvanised sheet you join by MIG braze welding with a copper filler, for example CuSi, without burning off the zinc coating.
In serial production and in a metalwork shop the job memory counts: you save up to 80 of your own JOB programs, each with a name of up to 16 characters, and you recall a proven technology with one button, without setting the parameters again at every changeover. The VJM mode (Variable Job Mode) adds the option of correcting saved settings when the assembly gap or the material batch changes. The machine goes to workshops, maintenance departments and production plants that work several kinds of material at one station. The Hold function keeps the last current and voltage values after the arc goes out, so you read the real bead parameters for the technology sheet.
Features and equipment
- Digitally controlled power stage instead of a stepped voltage switch: the setting is stepless and the circuit reacts at once to a change in arc length, so you match the dynamics to the given alloy.
- Synergic characteristics: the source itself ties the wire feed speed, the voltage, the pulse frequency and width and the base current, and you pick the working point.
- AluPlus, a double pulse with wide settings: modulation frequency, duty indicator, pulse height and pulse width, for shaping the penetration profile and the ripple on aluminium and CrNi.
- MIG/MAG Puls process: the droplet detaches at every current pulse, so metal transfer is free of spatter, the bead is cleaner and preparing the part after welding is shorter.
- SPAZ spatter free ignition: at the moment the wire touches the material the circuit lights a micro arc of about 8 A at about 10 V and only after it settles goes over to the main parameters, so the start of the weld needs no grinding and the contact tips live longer.
- JOB memory for up to 80 programs, with your own name of up to 16 characters: you recall the parameters for a part with one button.
- VJM mode (Variable Job Mode): you correct a saved program for a change of material or gap, without deleting the original settings.
- Working modes 2T, 4T and Super-4T: Super-4T has separate settings for the start, hot or gentle, and for crater filling at the end of the bead.
- Spot mode with a timer and External mode: the spot mode gives repeatable tacks, and External plugs the source into a mechanised station.
- Closed loop wire drive with a tachogenerator: a speed from 0 m/min to 24 m/min is held in spite of the resistance in the torch liner.
- Upper panel with LED displays of current, voltage, wire speed and program number, with the Hold function: after welding the values stay on the screen, so you read them for the documentation.
- Lower MC4 digital panel with a text display and icons: you program the whole cycle, that is gas pre flow, slope up, main current, slope down, wire burn back and gas post flow.
- Plug and Weld: after start-up the machine recognises the connected welding accessories.
- Gas pre flow and post flow time adjustment: the shield is ready before the arc appears and stays over the cooling crater, which on high alloy steels and aluminium decides the look and the soundness of the weld.
- MIG braze welding with CuSi or CuAl copper filler: you join galvanised sheet at a lower temperature, so the zinc coating stays in place and the joint does not rust from below.
- Compact housing joining the source and the feeder: one unit of about 600 x 270 x 470 mm instead of two boxes.
Technical data
| Brand | Cloos |
|---|---|
| Manufacturer and model | Carl Cloos Schweisstechnik GmbH, GLC 333 MC4 |
| Type | inverter MIG/MAG welder with MC4 digital control |
| Supply voltage | 3 x 400 V, 50 Hz |
| Mains fuse | T16 A |
| Welding current in the product record | up to 400 A |
| Welding current range | from 5 A at 14 V to 330 A at 31 V |
| Current at a 40% duty cycle | 330 A at 31 V |
| Current at a continuous 100% load | 260 A at 27 V |
| Open circuit voltage | 60 V |
| Wire feed speed | from 0 m/min to 24 m/min, drive controlled by a tachogenerator |
| Program memory | up to 80 JOB jobs |
| Protection class and insulation class | IP23, class F |
| Source cooling | Kühlart F, forced air circulation |
| Cooling in the product record | liquid |
| Source dimensions | about 600 x 270 x 470 mm |
| Source weight | from about 35 kg to 38 kg |
| Build standard | EN 60974-1, CE marking and the S mark |
| Processes | MIG/MAG, synergy, pulse, AluPlus double pulse, MIG braze welding |
What to watch out for
The machine needs a 3 x 400 V mains at 50 Hz and a T16 A fuse, and the open circuit voltage is 60 V. The housing has protection class IP23 and insulation class F, so it takes the dust and damp of a hall, but not washing with a jet. The source weighs from about 35 kg to 38 kg at dimensions of about 600 x 270 x 470 mm, so you move it without a pallet truck, although with a cylinder and accessories the station gets heavier. Plan the duty cycle by the documentation: you get 330 A at 40%, and without breaks the machine gives 260 A.
The cooling of the source itself is by air, in the forced Kühlart F system, while the product record gives liquid cooling, which refers to the torch configuration. Machines from the second hand market come in different configurations, so confirm the torch, the feeder rolls and any cooler module with us before you buy. The record puts the unit in the band up to 400 A, the model documentation speaks of 330 A. For aluminium prepare U type rolls and a PTFE liner, because AluPlus alone will not replace a proper wire path.
How we sell used machines
This unit was checked in our service workshop in Krotoszyn with measurements to PN-EN 60974-4 and a load test. The price includes the first year of the basic service package: an inspection with cleaning of the machine and a validation measurement. Further years can be added. We ship across the European Union, collection in person by appointment.